logotype
  • HOME
  • WHO WE ARE
    • ABOUT US
    • LEADERSHIP
    • CAPABILITIES
    • POLICIES
  • WHAT WE DO
    • INDUSTRIES
    • APPLICATIONS
    • PRODUCTS
  • JOIN US
    • VENDORS
    • CAREERS
CONTACT US
logotype
logotype
  • HOME
  • WHO WE ARE
    • ABOUT US
    • LEADERSHIP
    • CAPABILITIES
    • POLICIES
  • WHAT WE DO
    • INDUSTRIES
    • APPLICATIONS
    • PRODUCTS
  • JOIN US
    • VENDORS
    • CAREERS
CONTACT US
logotype
  • HOME
  • WHO WE ARE
    • ABOUT US
    • LEADERSHIP
    • CAPABILITIES
    • POLICIES
  • WHAT WE DO
    • INDUSTRIES
    • APPLICATIONS
    • PRODUCTS
  • JOIN US
    • VENDORS
    • CAREERS
Contact Us
Portfolio
HomeApplicationsSulphur Recovery Unit

Sulphur Recovery Unit

0
TPH
0
kg/cm2
0
°C
0 +
units
SULPHUR RECOVERY

Packages for the Claus unit.

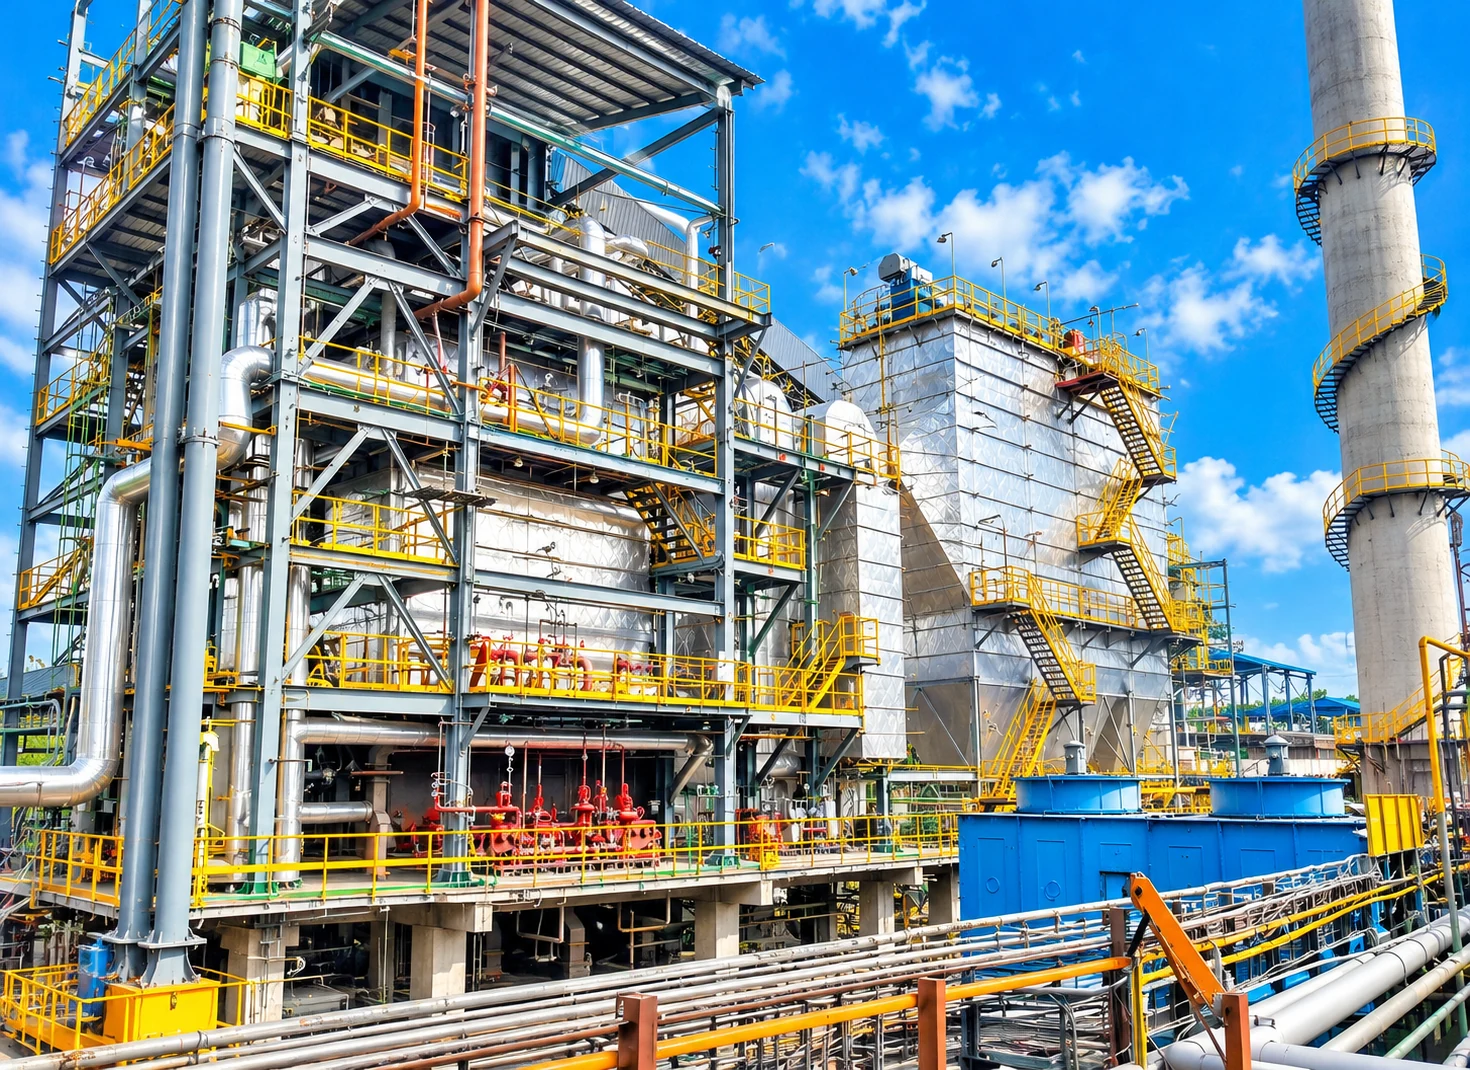
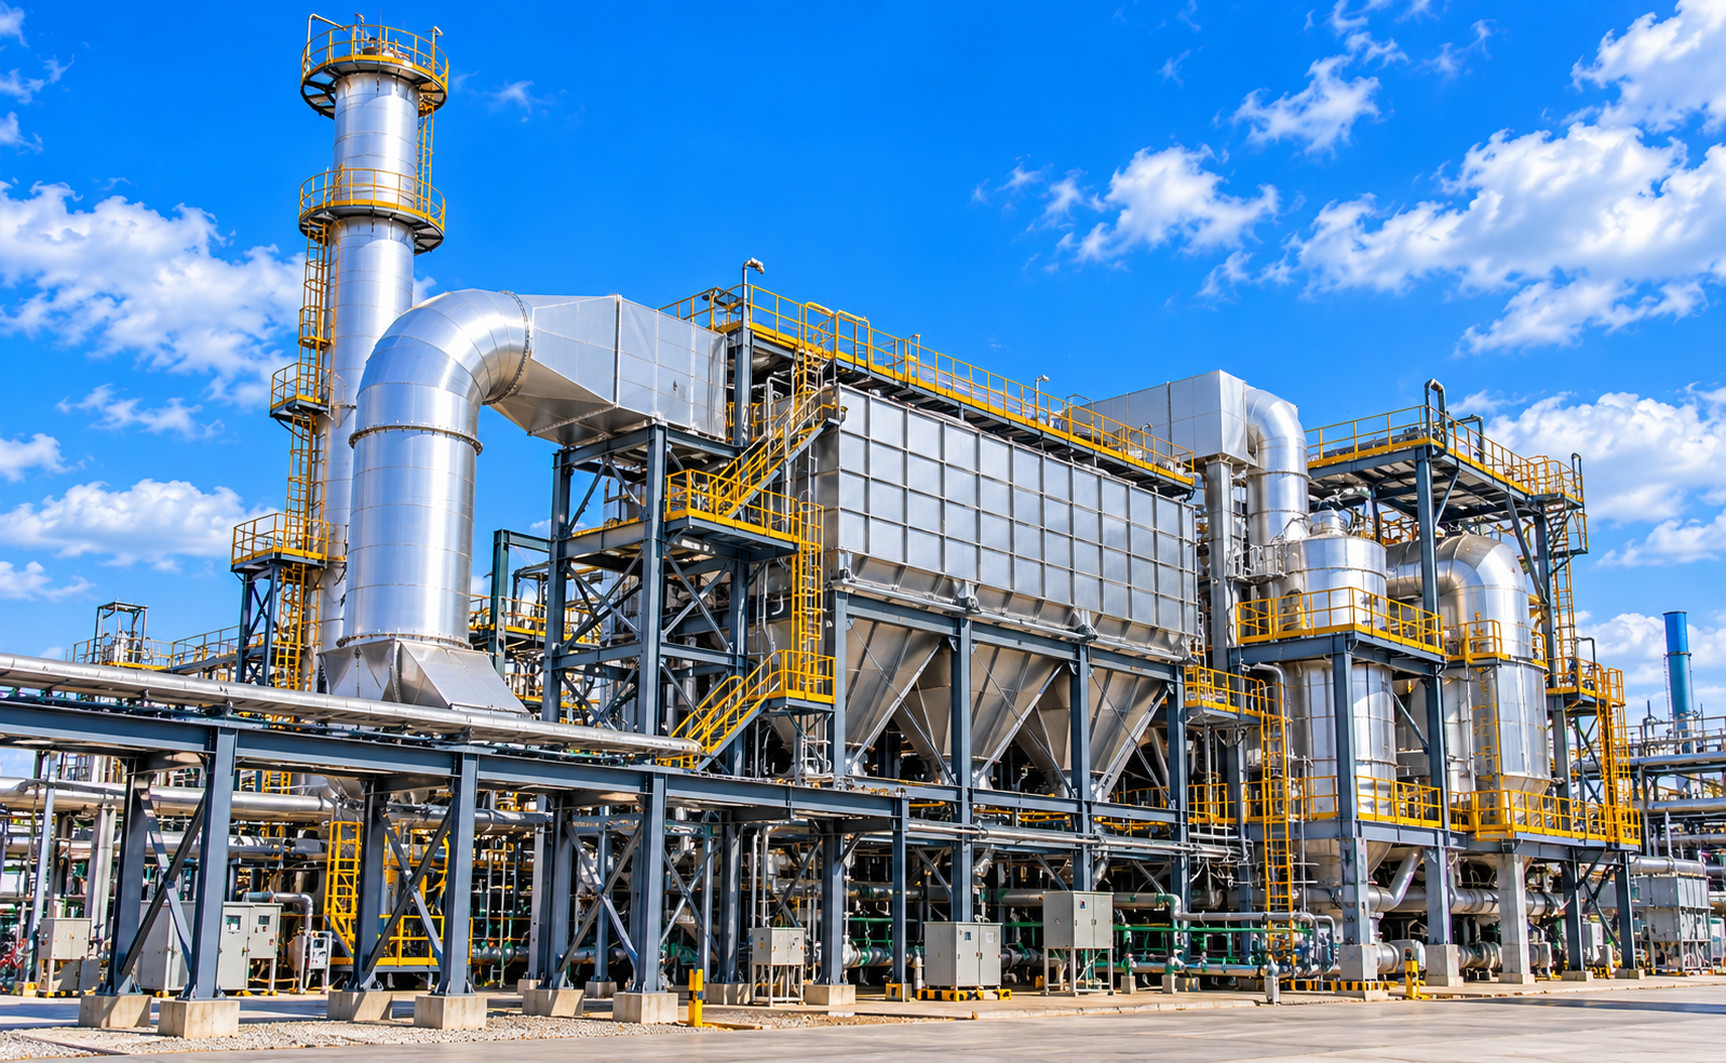
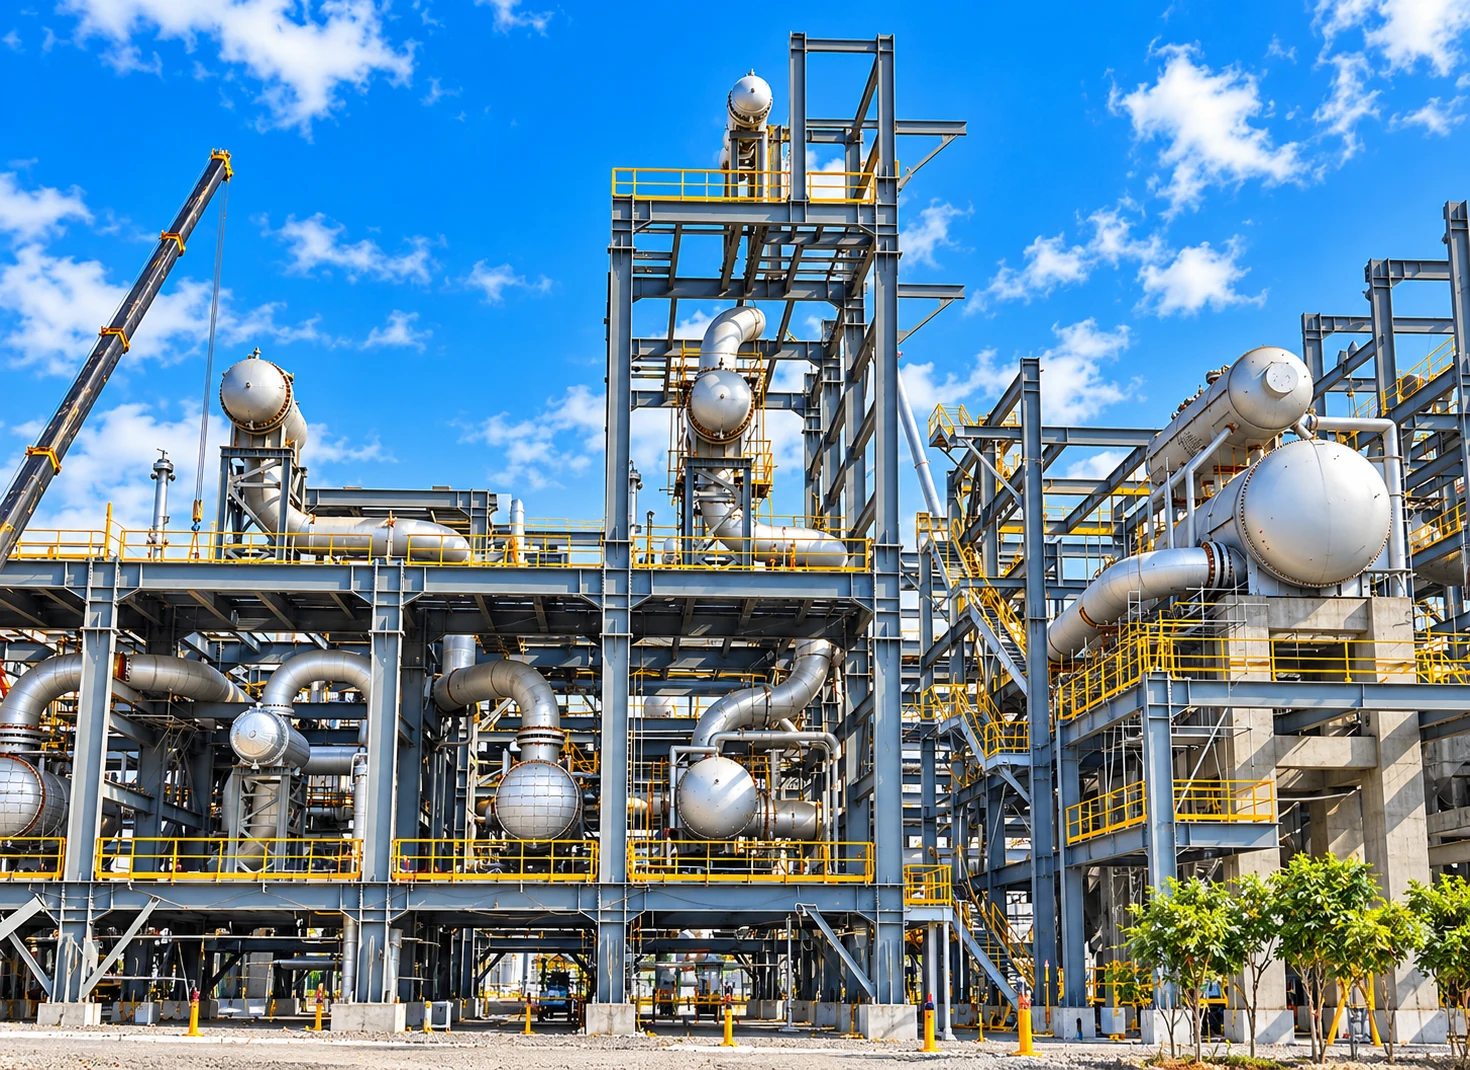
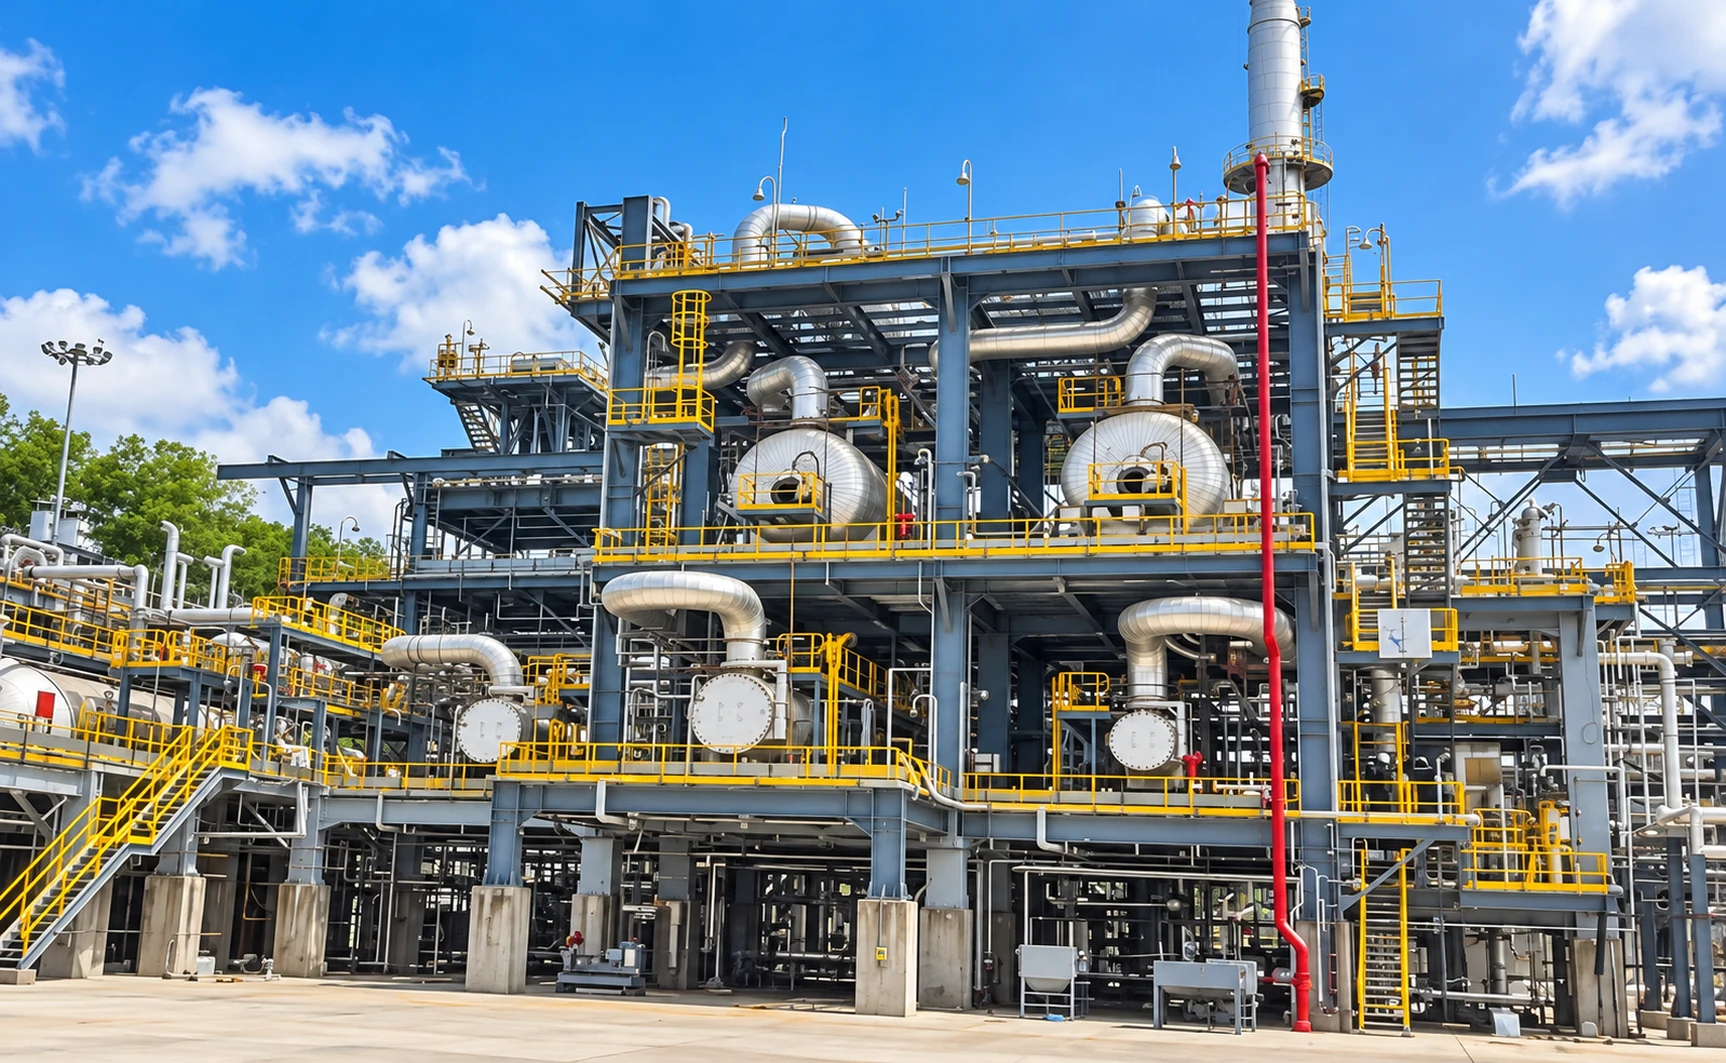
A sulphur recovery unit converts hydrogen sulphide into elemental sulphur in a reaction furnace, a waste heat boiler, condensers and catalytic reactors. We build the whole train, and we are a pioneer of Claus packages in India.

Where the heat is

Acid gas from the upstream units is burned with air in the reaction furnace at 950 to 1,300 °C, forming sulphur dioxide that reacts with the remaining hydrogen sulphide to make sulphur. The hot gas is quenched in a waste heat boiler that raises high-pressure steam, then cooled in a condenser to drop out liquid sulphur. Two or three catalytic reactors, each followed by a condenser, convert what remains, and a tail gas incinerator destroys the rest before the stack.

What the equipment has to do

  • Reaction furnace and waste heat boiler form one unit, the MCC package, designed for refractory life, tube protection at the inlet and steam at the refinery's conditions
  • Condensers cool to just above the sulphur dew point and drain liquid sulphur without plugging
  • Reactors hold the catalyst at reaction temperature
  • The incinerator reaches destruction temperature and recovers its heat
What we supply

  • Major references across the globe, including one of India's largest SRUs
  • MCC packages: combustion chamber, waste heat boiler, sulphur condensers and reactors
  • Incinerator packages: incinerator chamber, waste heat boiler and superheater
  • TGTU packages: combustion chamber and waste heat boiler for tail gas treating
  • Fire-tube or water-tube construction, modular for site assembly, to the licensor's basis

Our Industrial Products
MCC Package

Combustion chamber, waste heat boiler, sulphur condensers and reactors as one package.

Incinerator Package

Incinerator chamber, waste heat boiler and superheater for the tail gas.

TGTU Package

Combustion chamber and waste heat boiler for the tail gas treating unit.

Thermal Systems provides MCC & Incinerator WHB packages for SRU in refinery

  • Fire Tube / Water Tube construction of WHB

  • Modular construction for ease of site assembly

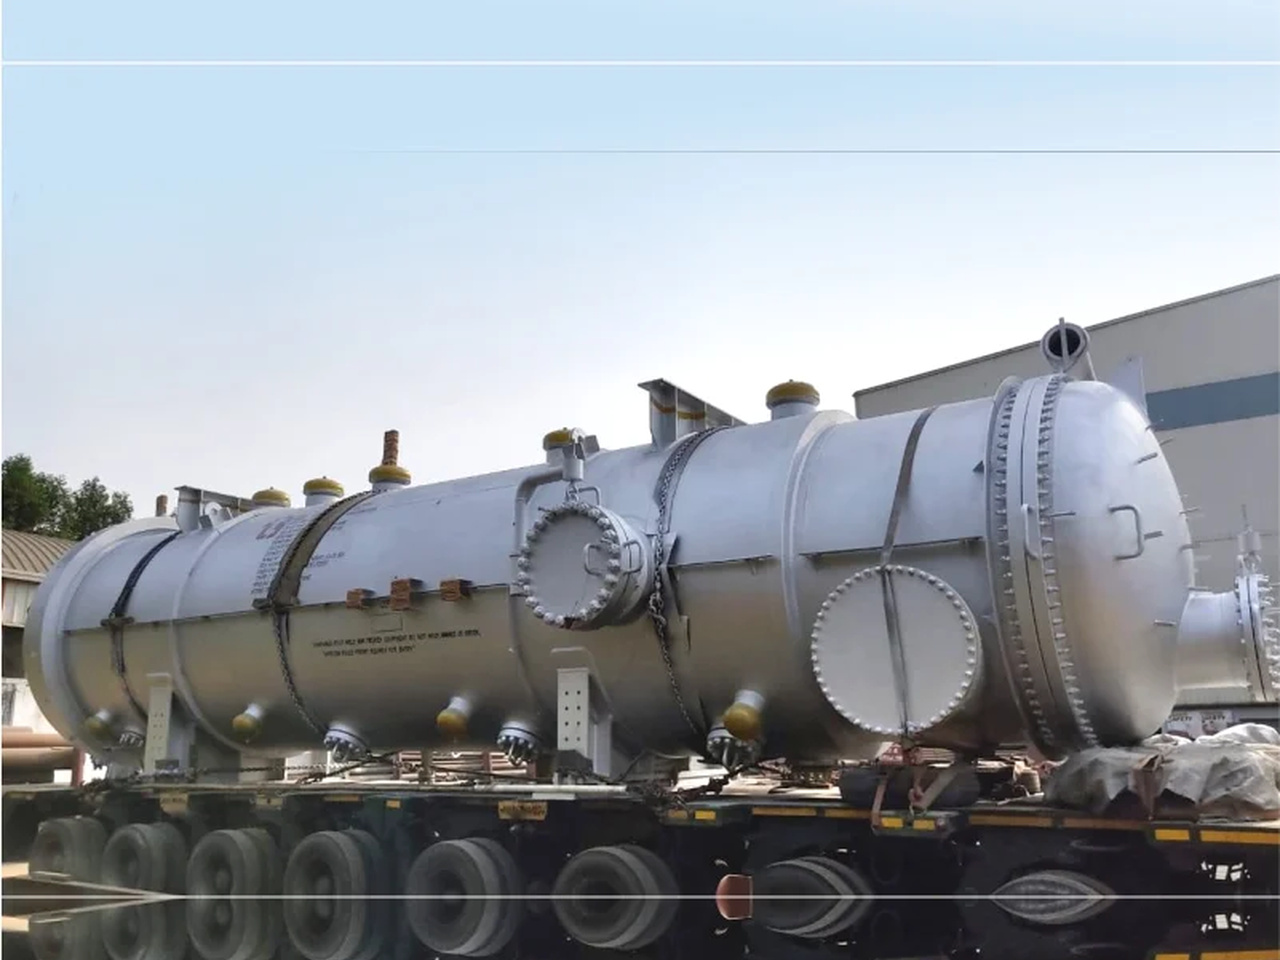
  • Reaction Furnace (MCC) package for SRU

  • Incinerator Package for SRU

India’s leading manufacturer having highest number of successful installations for SRU application in major refineries

Reaction Furnace (Mcc) Package

For Sulphur Recovery Unit

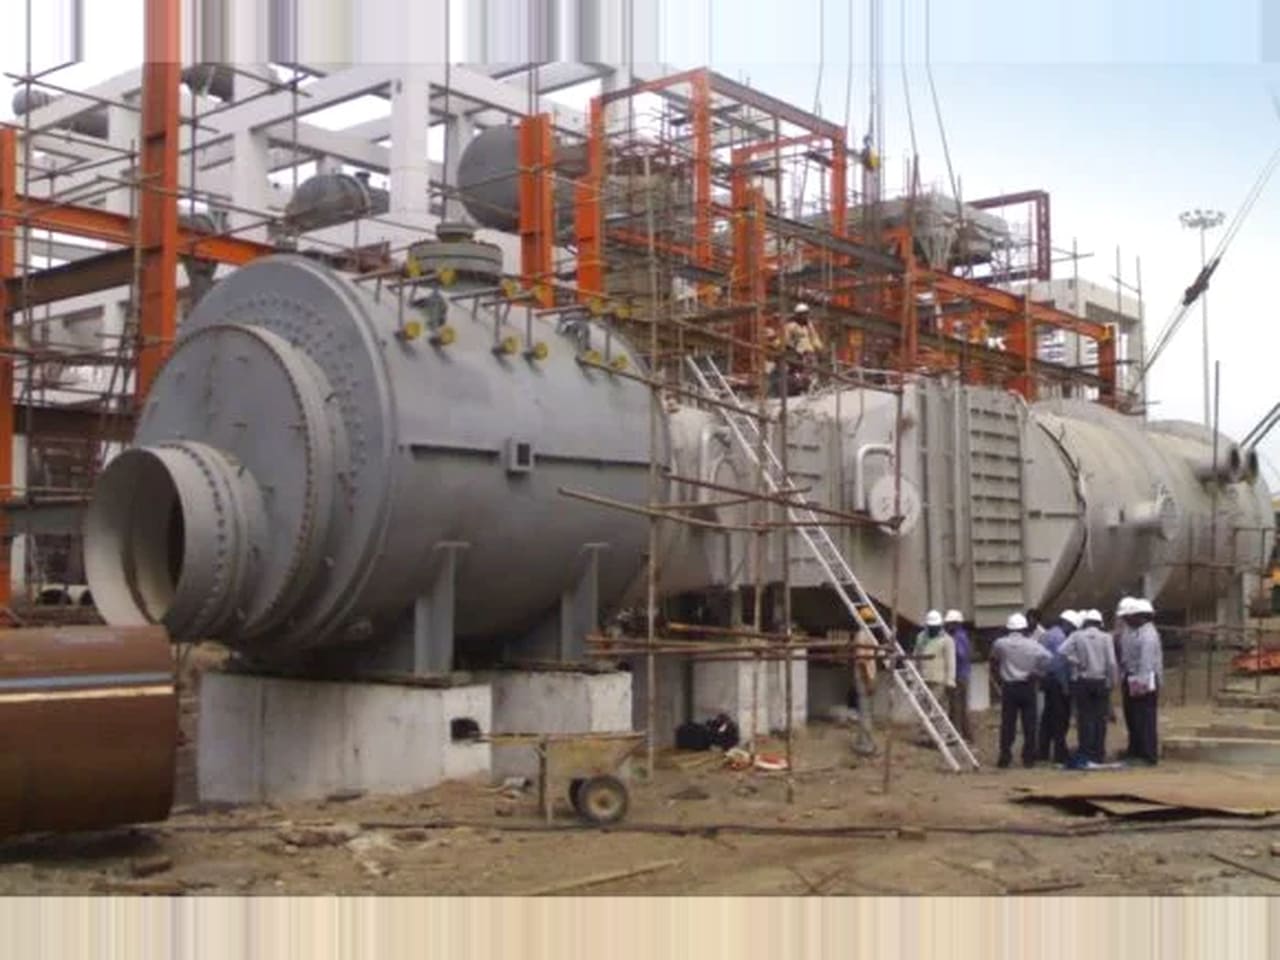
In the Claus process, H2S-rich acid gas is burned in the reaction furnace, generating gas at around 1,300 °C. The furnace outlet gas is quenched in the MCC waste heat boiler, generating HP/MP steam.

Thermal Systems supplies complete Reaction Furnace (MCC) packages — burner, chamber, boiler and EBOP — in fire tube construction, with superheaters suitable for internal and import steam.
 
DOWNLOAD BROCHURE

Incinerator Package

For Sulphur Recovery Unit

Tail gas leaving the SRU is thermally incinerated before discharge. The hot incinerator flue gas is cooled in a waste heat recovery boiler of fire tube or water tube construction.

Thermal Systems’ incinerator packages are of modular construction for ease of site assembly, with references including a 600 TPD SRU at Essar, Vadinar.

Tail Gas Treatment Unit Package

For Sulphur Recovery Unit

In tail gas treatment units, the treated gas stream is incinerated and its heat recovered in a waste heat boiler cum superheater.

Thermal Systems has supplied TGTU packages including 2 × 100 TPD TGTU boilers at HPCL Mumbai.

PREV

Spent Acid Regeneration Units

NEXT

Methanol

Leave a Reply Cancel reply

Your email address will not be published. Required fields are marked *

Let's Convert Your Vision Into Reality

We support our clients throughout the entire project cycle – from identifying needs to commissioning, employing all our professional expertise in the most challenging contexts

Contact us

Get Social:

Linkedin

Quick Links

  • Home
  • About Us
  • Contact Us
  • Leadership
  • Capabilities

Explore Us

  • Industries
  • Applications
  • Products
  • Vendors
  • Policies

Address

  • Thermal Systems (Hyderabad) Pvt Ltd. Plot No.158, IDA Bollaram, Sangareddy, Hyderabad, Telangana, India
  • info@thermalindia.com

Get Social:

Linkedin

© 2026 Thermal Systems (Hyderabad) Pvt. Ltd. All Rights Reserved.

  • Privacy Policy
  • Terms & Conditions

Driven by passion. Grounded in purpose. Focused on results.

aerra@mail.com
+1 800 123 46 57
X-twitterFacebookInstagramLinkedin

Useful Links

  • Company
  • Services
  • Features
  • FAQs
  • Getting Started

Subscribe

Our expertise, as well as our passion for web design, sets us apart from other agencies.

© 2026 Aerra byWebGeniusLab. All Rights Reserved