MCC PACKAGE
The front end of the sulphur recovery unit.
Combustion chamber, waste heat boiler, sulphur condensers and reactors, delivered as one
REFORMED GAS IN up to 920°C
PROCESS GAS BOILER
STEAM 68 kg/cm²
CAPACITY up to 128 TPH
135 TPH
74 kg/cm²
490°C
55+ units
What it is
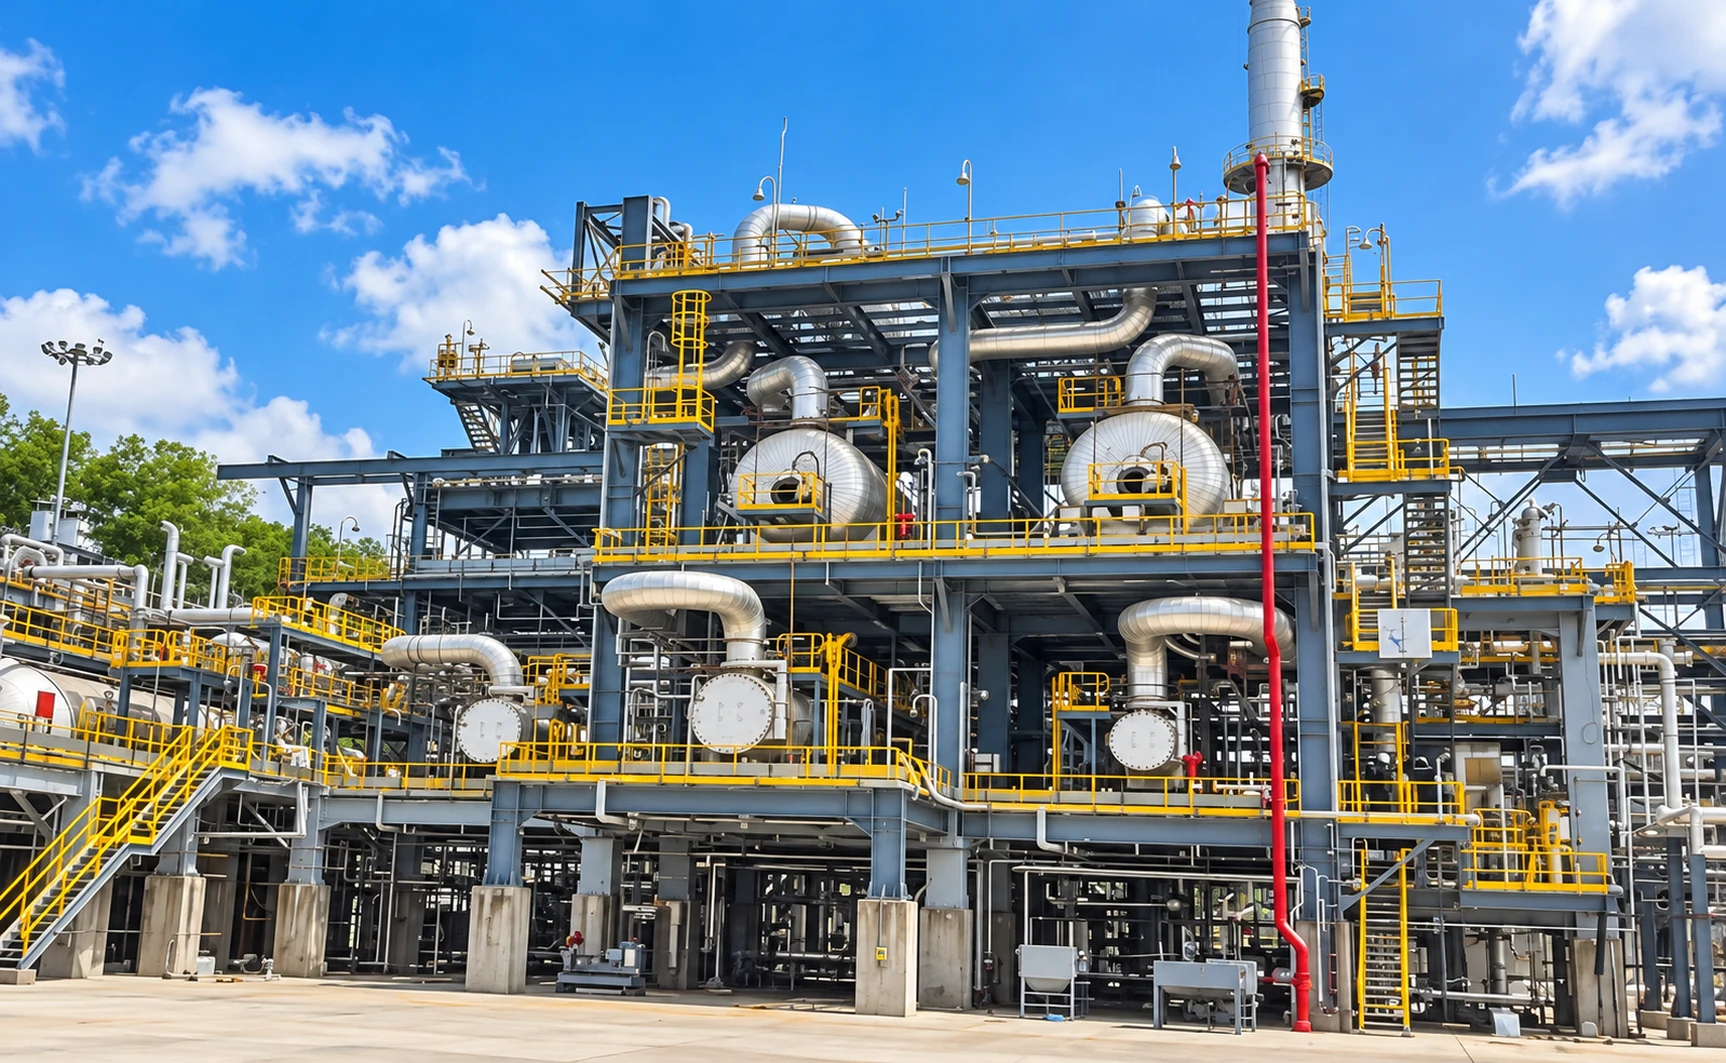
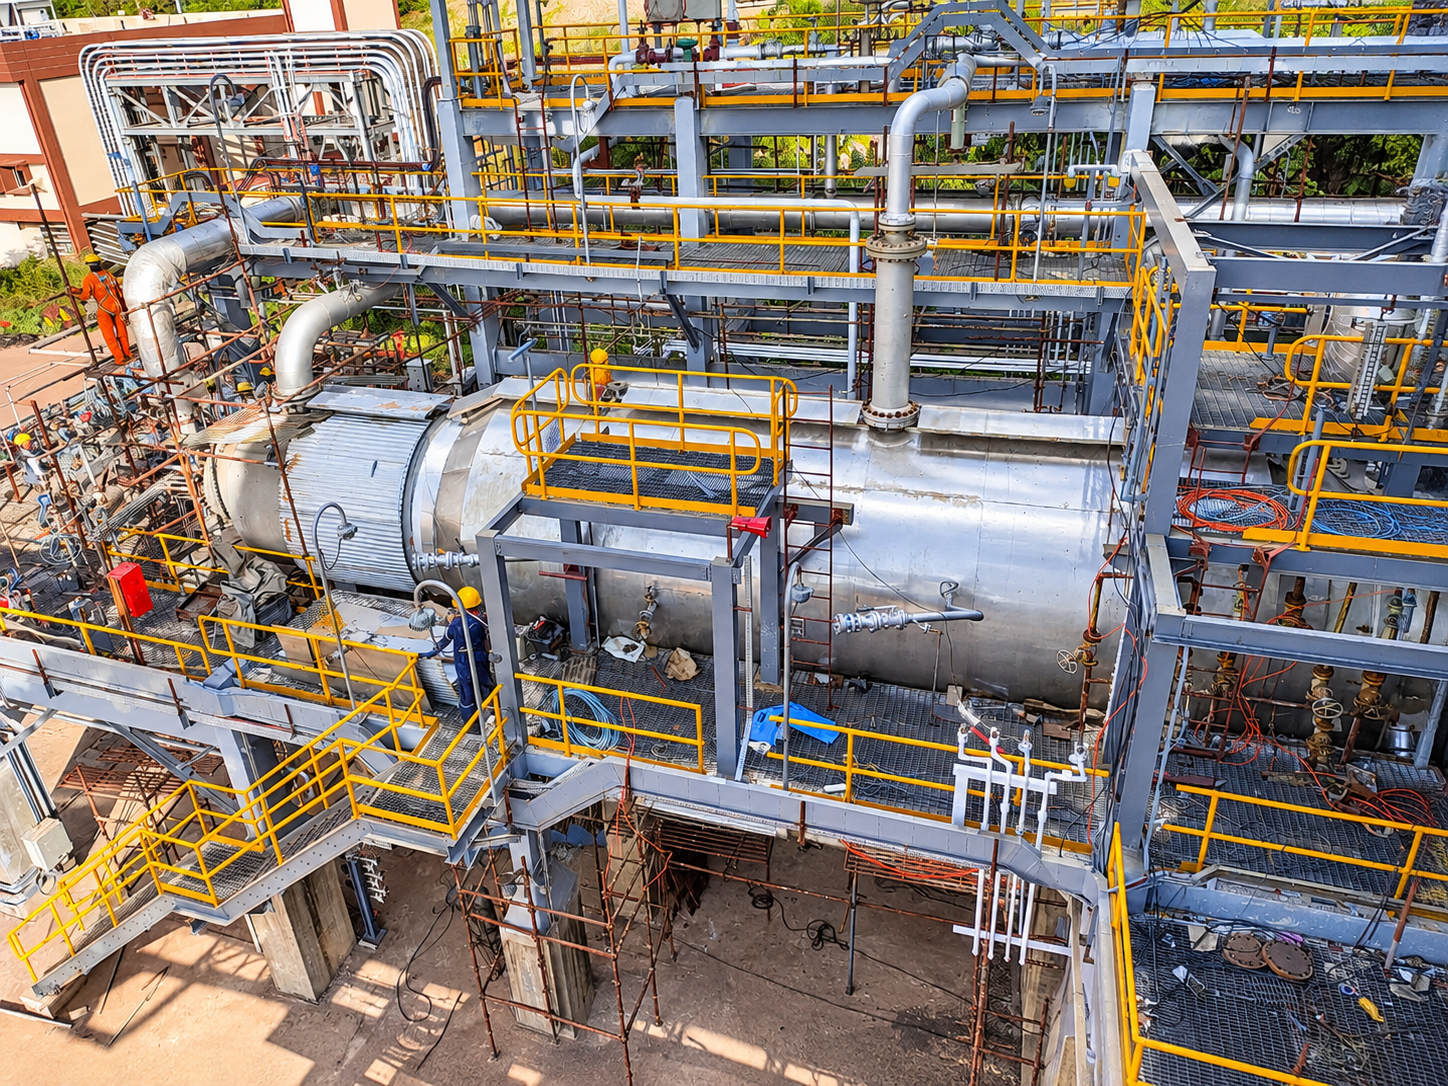
In a Claus unit the acid gas is burned in a refractory-lined combustion chamber at 950 to 1,300 °C and immediately quenched in a waste heat boiler. The gas is then cooled in sulphur condensers that drain liquid sulphur, and converted further in catalytic reactors. We supply the whole front end as a main combustion chamber package: combustion chamber with refractory and burner interface, waste heat boiler with protected tube inlets, steam drum, sulphur condensers and Claus reactors, engineered to the licensor's basis and built in modules for site assembly.
- Fire Tube / Water Tube construction of WHB
- Modular construction for ease of site assembly
- Reaction Furnace (MCC) package for SRU
- Incinerator Package for SRU


How we build it
- Combustion chamber shell with refractory lining and burner interface to licensor design
- Waste heat boiler in fire-tube or water-tube construction with inlet protection
- Kettle-type sulphur condensers with low-pressure steam generation and sulphur drain design against solidification
- Claus reactors with catalyst support, inlet distribution and refractory or insulation as required
- Steam drum and circulation for high-pressure steam
- Modular construction for ease of site assembly; built under ASME U and S stamps with full documentation
REACTION FURNACE (MCC) PACKAGE
For Sulphur Recovery Unit
In the Claus process, H2S-rich acid gas is burned in the reaction furnace, generating gas at around 1,300 °C. The furnace outlet gas is quenched in the MCC waste heat boiler, generating HP/MP steam.
Thermal Systems supplies complete Reaction Furnace (MCC) packages — burner, chamber, boiler and EBOP — in fire tube construction, with superheaters suitable for internal and import steam.
TAIL GAS TREATMENT UNIT PACKAGE
For Sulphur Recovery Unit
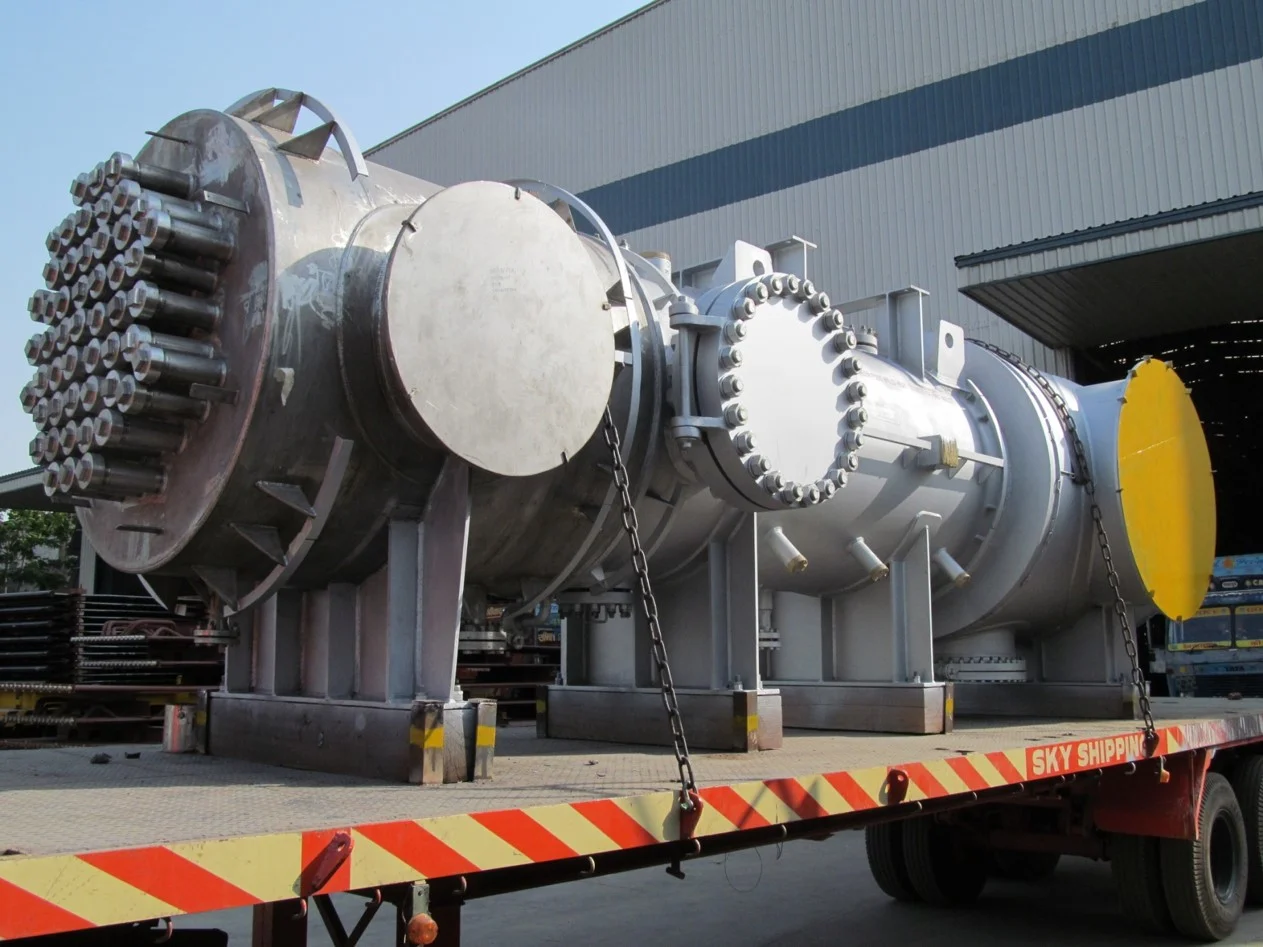
In tail gas treatment units, the treated gas stream is incinerated and its heat recovered in a waste heat boiler cum superheater.
Thermal Systems has supplied TGTU packages including 2 × 100 TPD TGTU boilers at HPCL Mumbai.

