INCINERATOR PACKAGE
Destroy the gas, keep the heat.
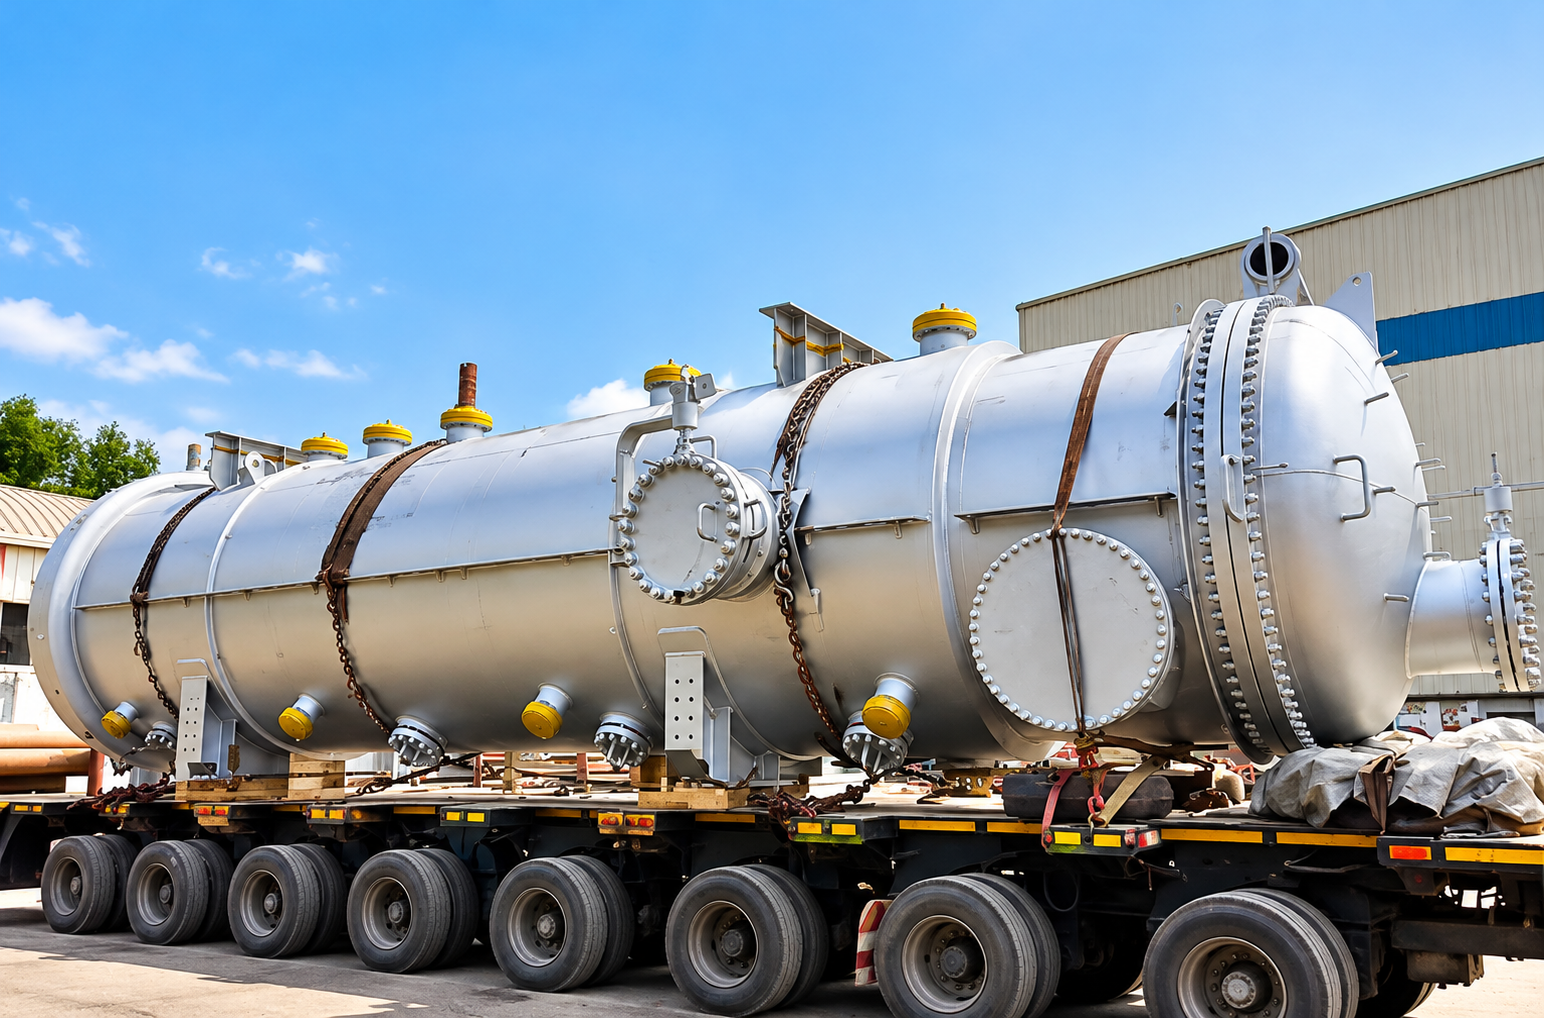
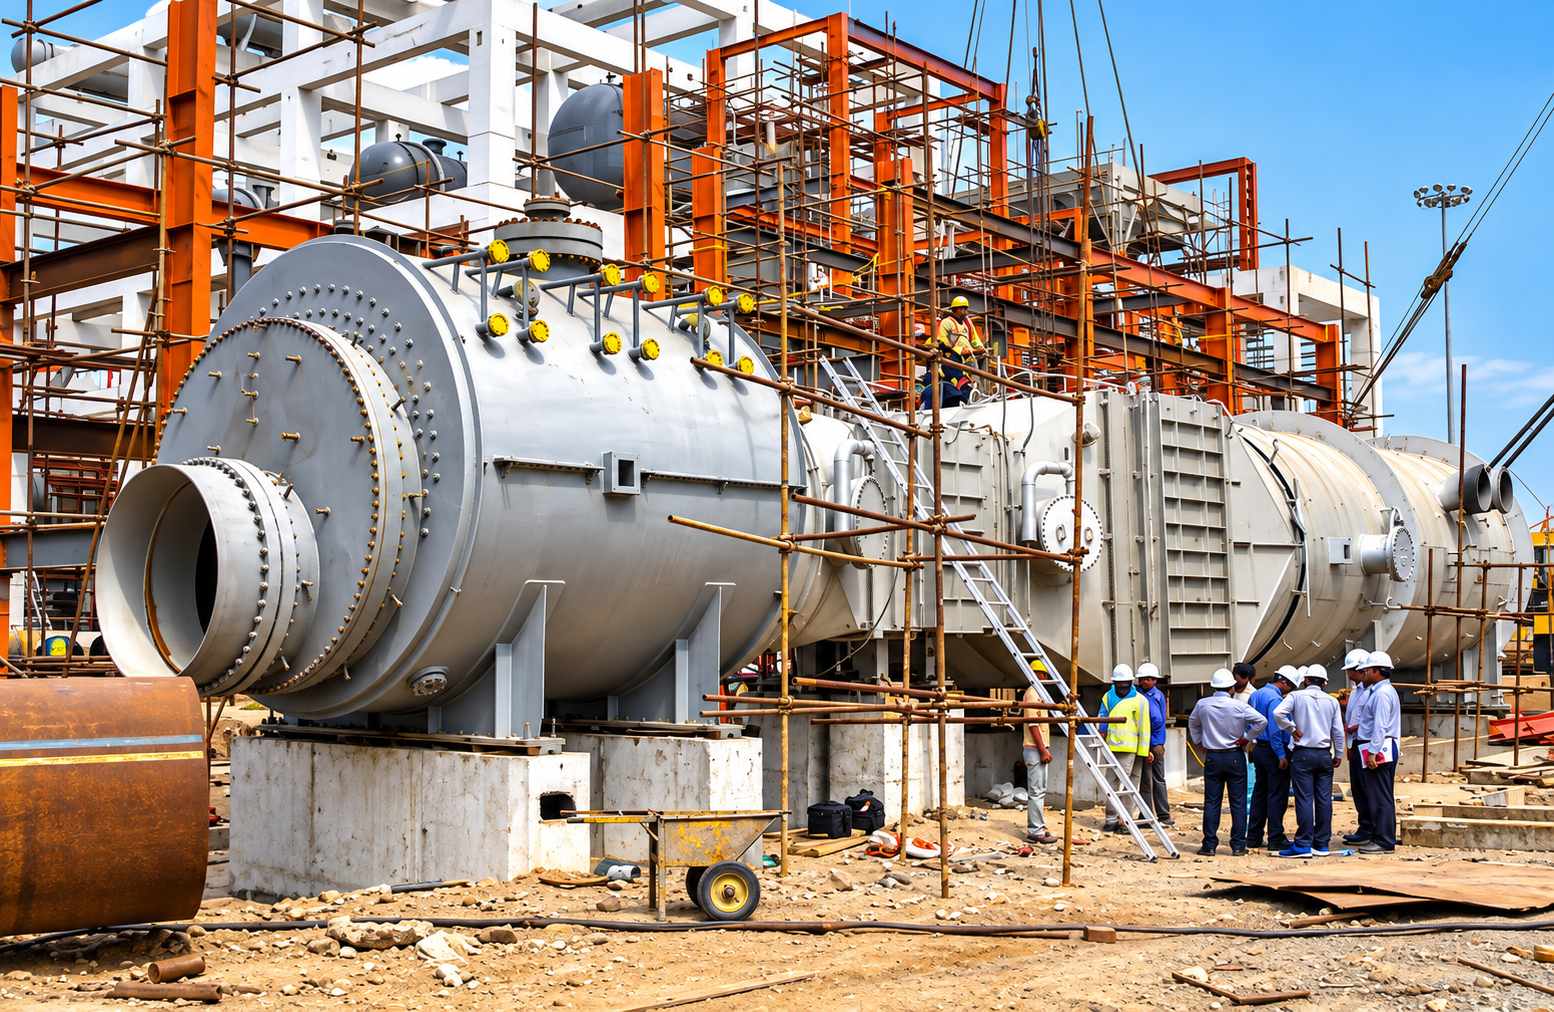
Incinerator chamber, waste heat boiler and superheater as one package, for sulphur unit tail gas and for liquid and gaseous industrial wastes.

128 TPH
Largest unit capacity
68 kg/cm²
Steam pressure
284 °C
Steam temperature
27
Installations in hydrogen units
What it is
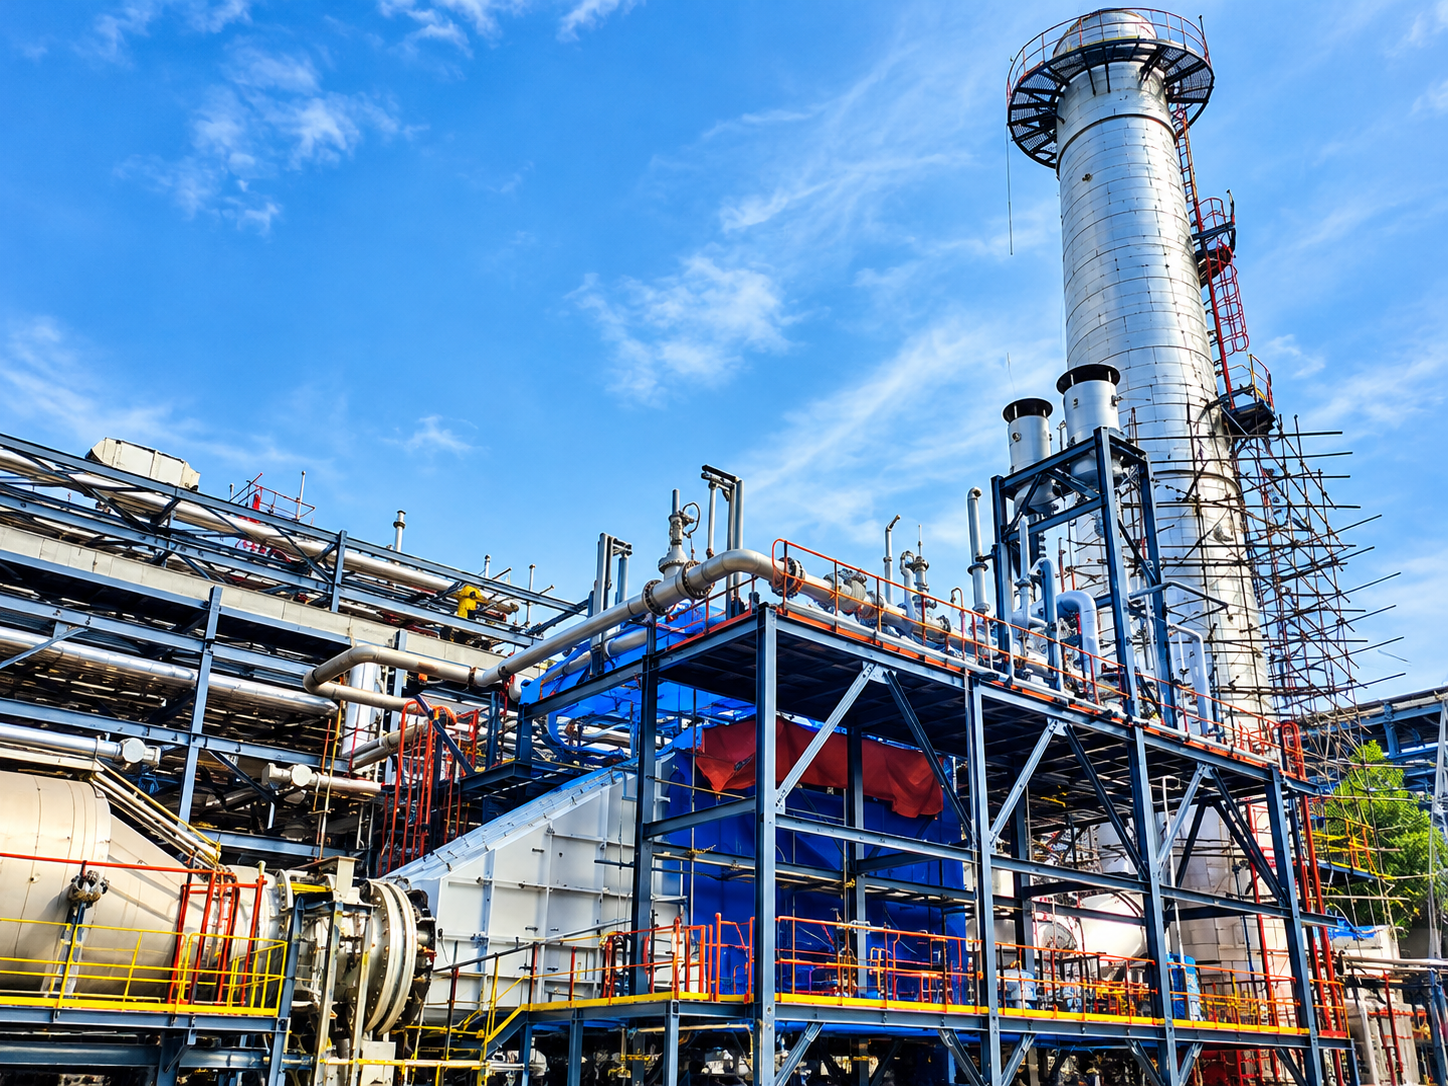
The tail gas of a sulphur recovery unit, and the liquid and gaseous wastes of chemical, pharmaceutical and petrochemical plants, are destroyed in a refractory-lined incinerator chamber with an auxiliary burner, at a temperature and residence time that the regulations define. The heat released is recovered in a waste heat boiler behind the chamber and raised to turbine or process conditions in a superheater. We engineer the chamber, the burner interface, the boiler and the superheater as one system, so that destruction temperature, residence time and steam output are designed together.

How we build it
- Refractory-lined incinerator chamber with burner interface and auxiliary fuel
- Waste heat boiler in fire-tube or water-tube construction, designed with the chamber for the required residence time
- Superheater for turbine or process steam conditions
- Tube metals and temperatures chosen for sulphur and chloride-bearing gas
- Open, cleanable gas path for salt and ash deposits
- Modular construction for site assembly; built under ASME U and S stamps