logotype
  • HOME
  • WHO WE ARE
    • ABOUT US
    • LEADERSHIP
    • CAPABILITIES
    • POLICIES
  • WHAT WE DO
    • INDUSTRIES
    • APPLICATIONS
    • PRODUCTS
  • JOIN US
    • VENDORS
    • CAREERS
CONTACT US
logotype
logotype
  • HOME
  • WHO WE ARE
    • ABOUT US
    • LEADERSHIP
    • CAPABILITIES
    • POLICIES
  • WHAT WE DO
    • INDUSTRIES
    • APPLICATIONS
    • PRODUCTS
  • JOIN US
    • VENDORS
    • CAREERS
CONTACT US
logotype
  • HOME
  • WHO WE ARE
    • ABOUT US
    • LEADERSHIP
    • CAPABILITIES
    • POLICIES
  • WHAT WE DO
    • INDUSTRIES
    • APPLICATIONS
    • PRODUCTS
  • JOIN US
    • VENDORS
    • CAREERS
Contact Us
Portfolio
HomeApplicationsSulphuric Acid Plant

Sulphuric Acid Plant

0
CAPACITY (TPH)
0
PRESSURE (kg/cm2)
0
TEMPERATURE (°C)
0 +
INSTALLATIONS
SULPHURIC ACID

Heat recovery in sulphuric acid production.

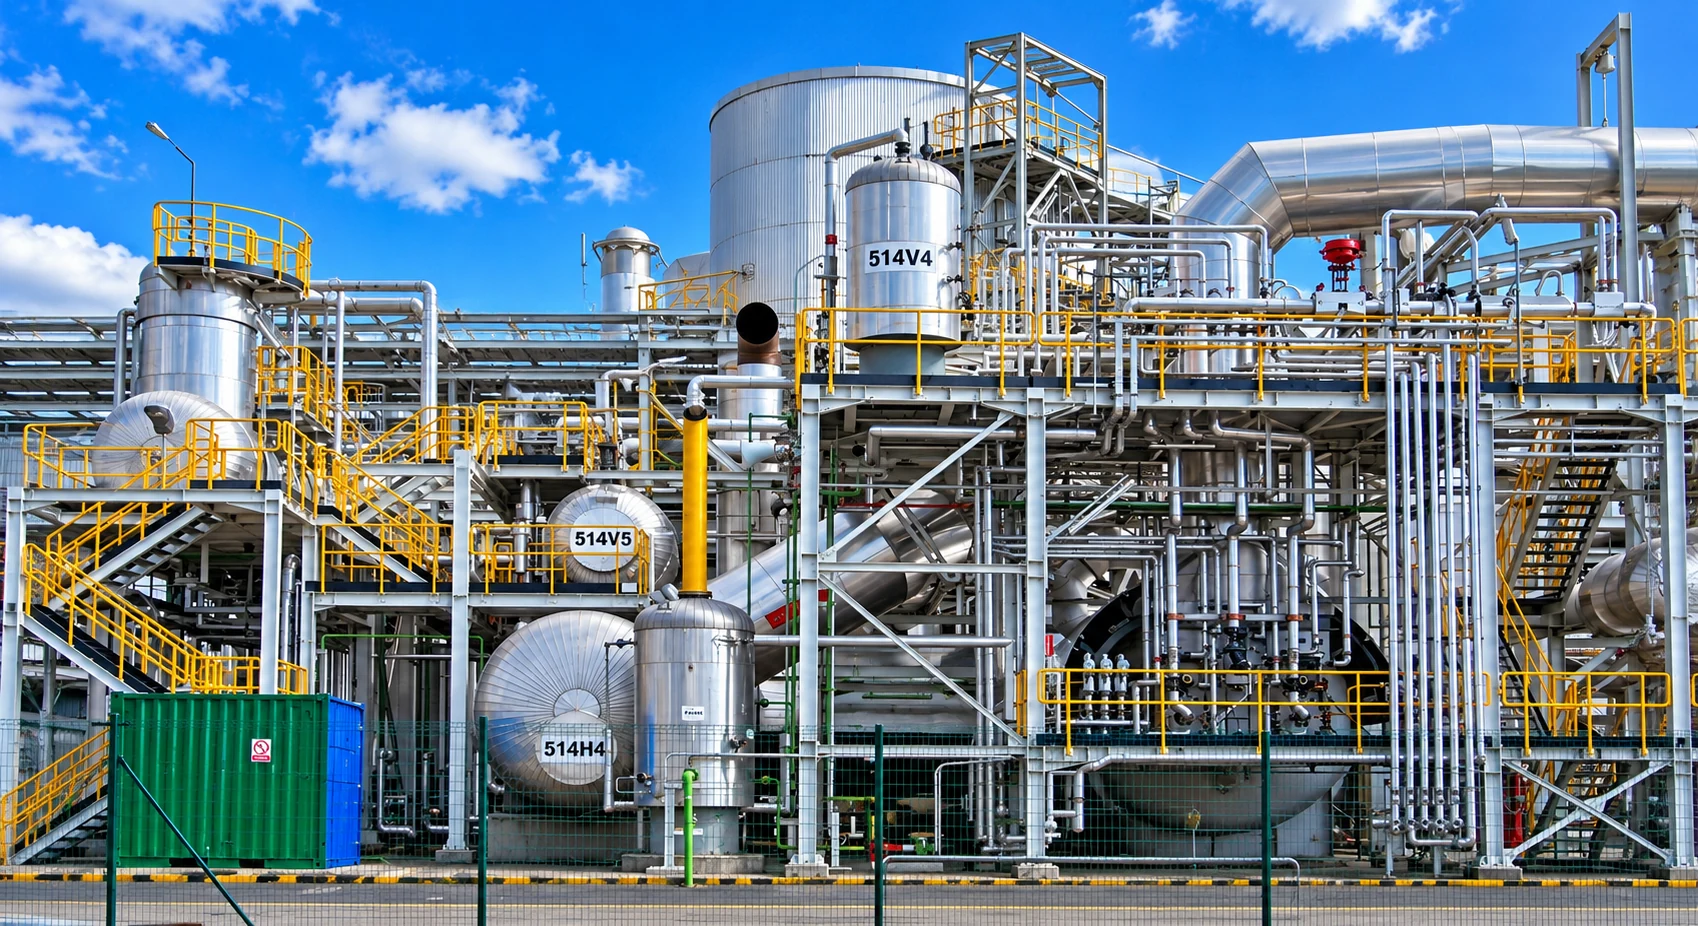
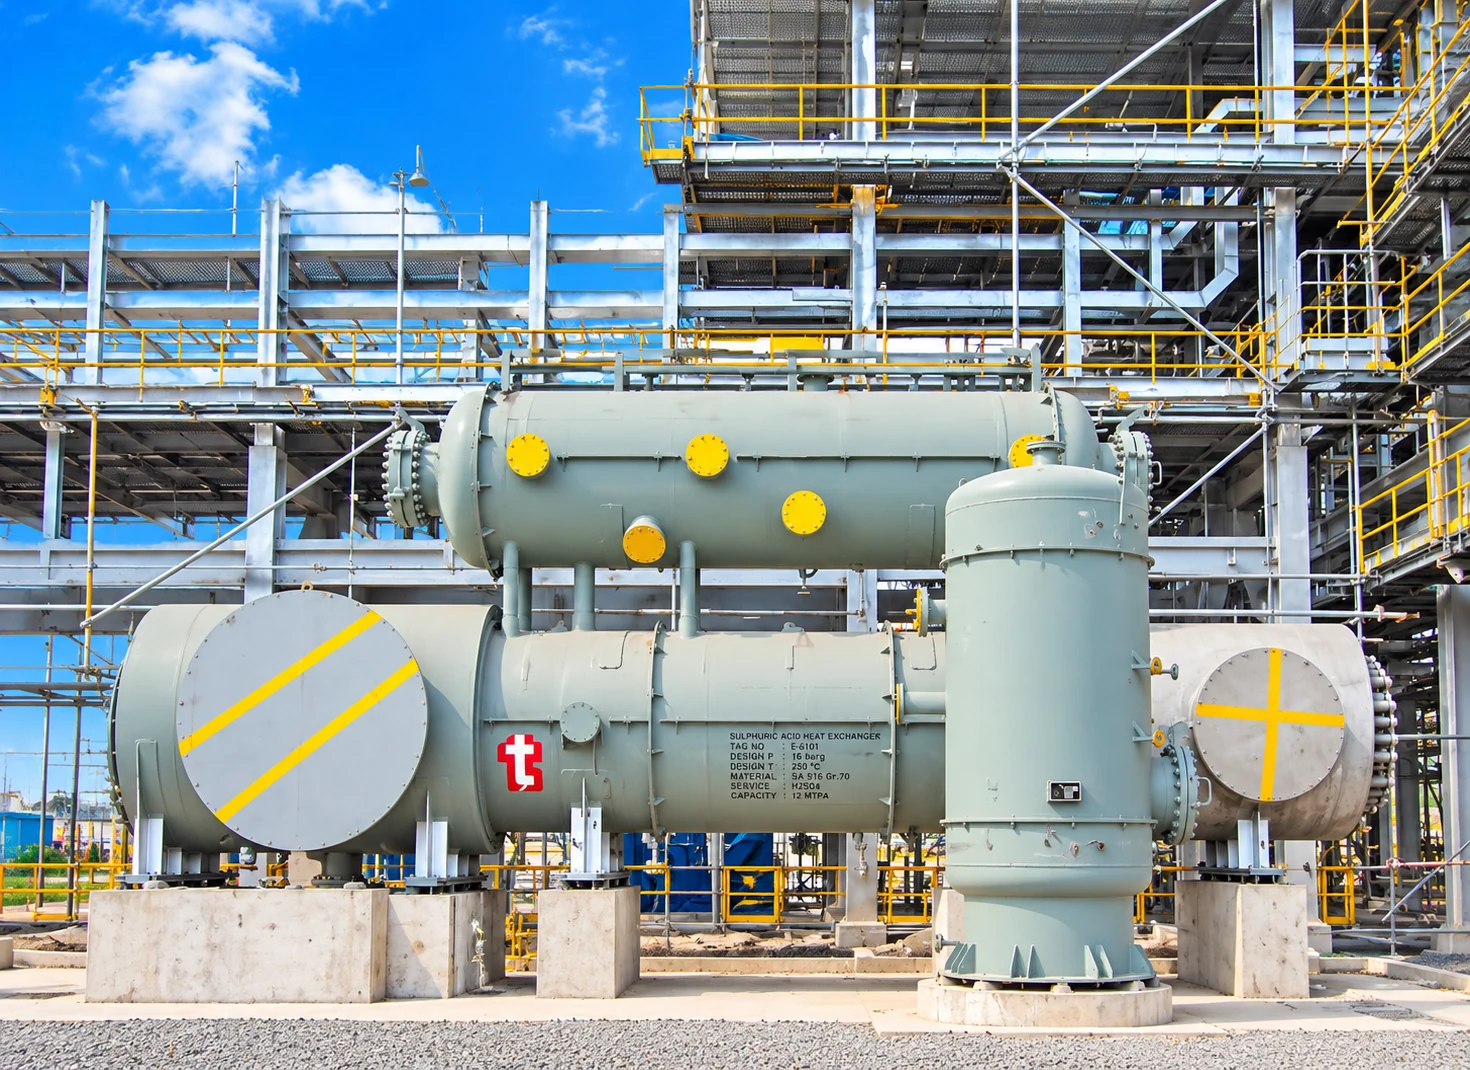
Sulphuric acid is the world's largest-volume chemical, and every plant that makes it from sulphur is a heat recovery plant first. We have supplied the boilers and exchangers for over 250 of them, for plants up to 5,000 TPD, and we have built boilers for one of the world's largest sulphuric acid plants.

Where the heat is

Molten sulphur is burned to sulphur dioxide, converted to sulphur trioxide over a catalyst, and absorbed to make acid. The sulphur furnace delivers gas at high temperature; the waste heat boiler cools it to the converter inlet and raises high-pressure steam. Between catalyst beds, gas-gas heat exchangers move heat from converted gas to incoming gas so that each bed runs at its design temperature; economisers and superheaters take the remaining heat. Acid can also be made from metallurgical off-gas or by regenerating spent acid, with the same heat recovery logic.

What the equipment has to do

  • Cool the gases to the temperatures the catalyst needs at each pass of the converter
  • Maximise steam without quenching the gas below the acid dew point
  • Fire-tube boilers with external and integral gas bypass for temperature control
  • Water-tube boilers with provision for expansion
  • Both built in modules for overseas shipment
What we supply

  • Waste heat boilers
  • Gas-gas heat exchangers
  • Preheaters
  • Economisers and superheaters
  • From concept to commissioning

Our Industrial Products
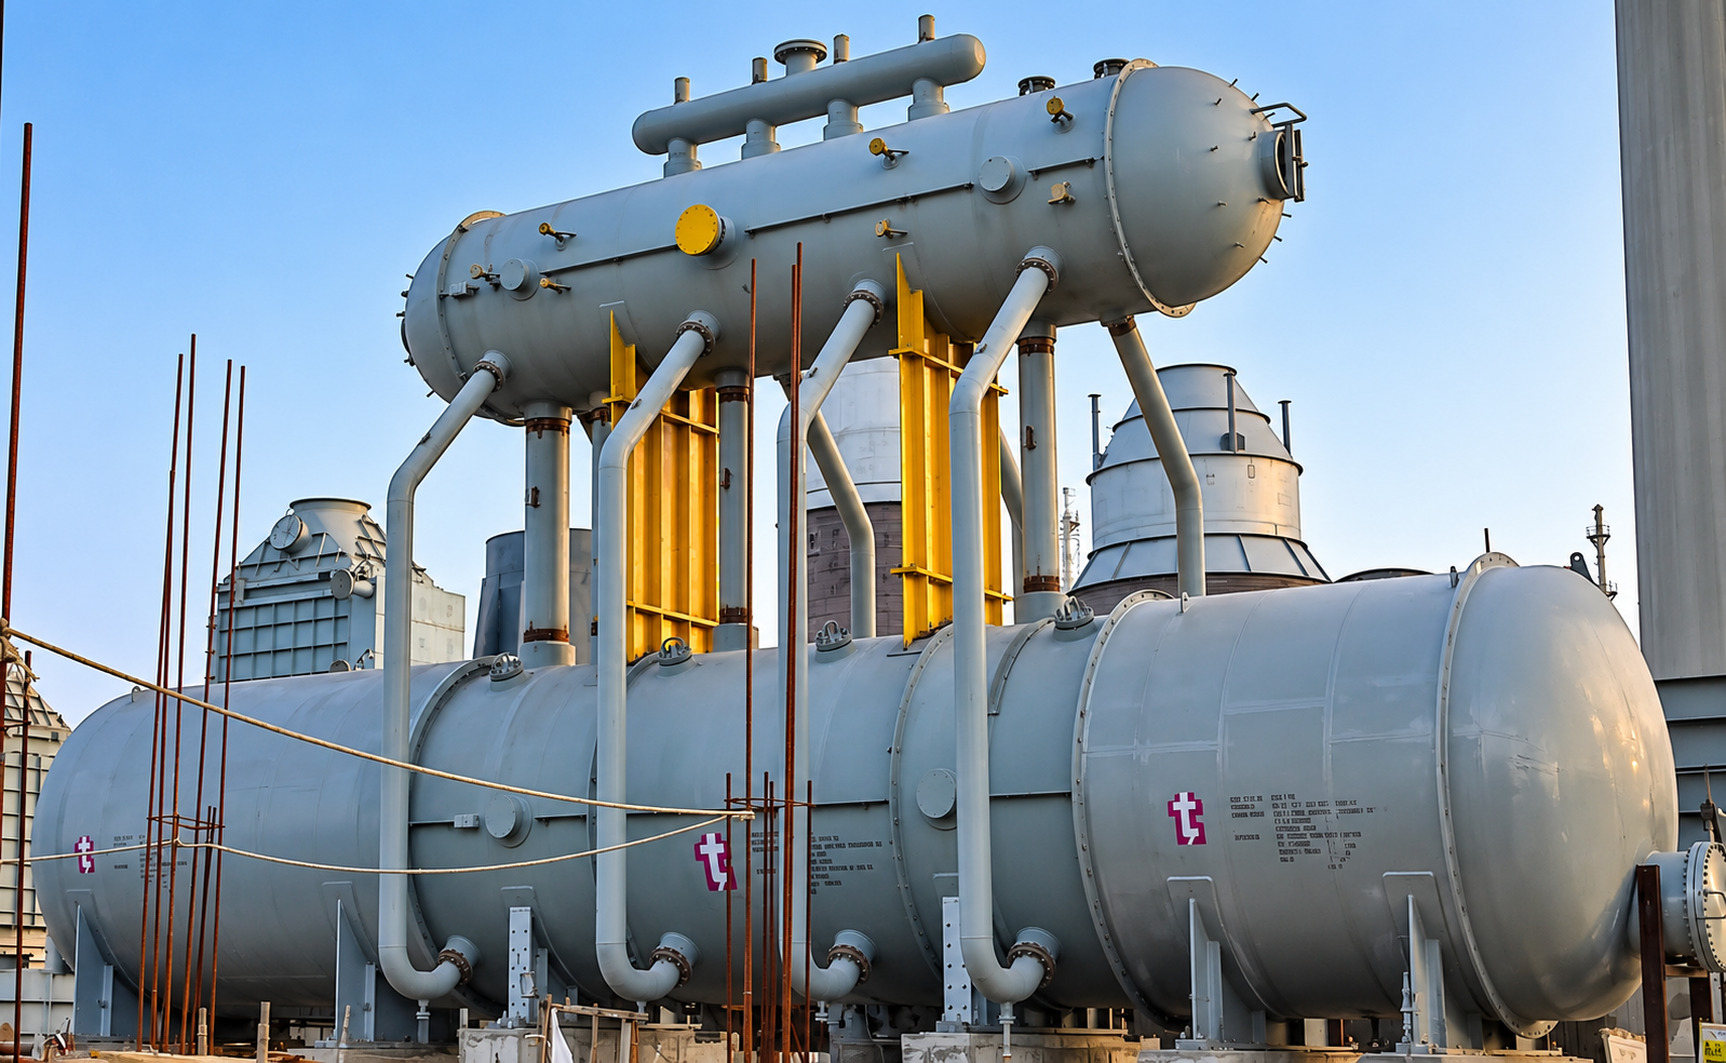
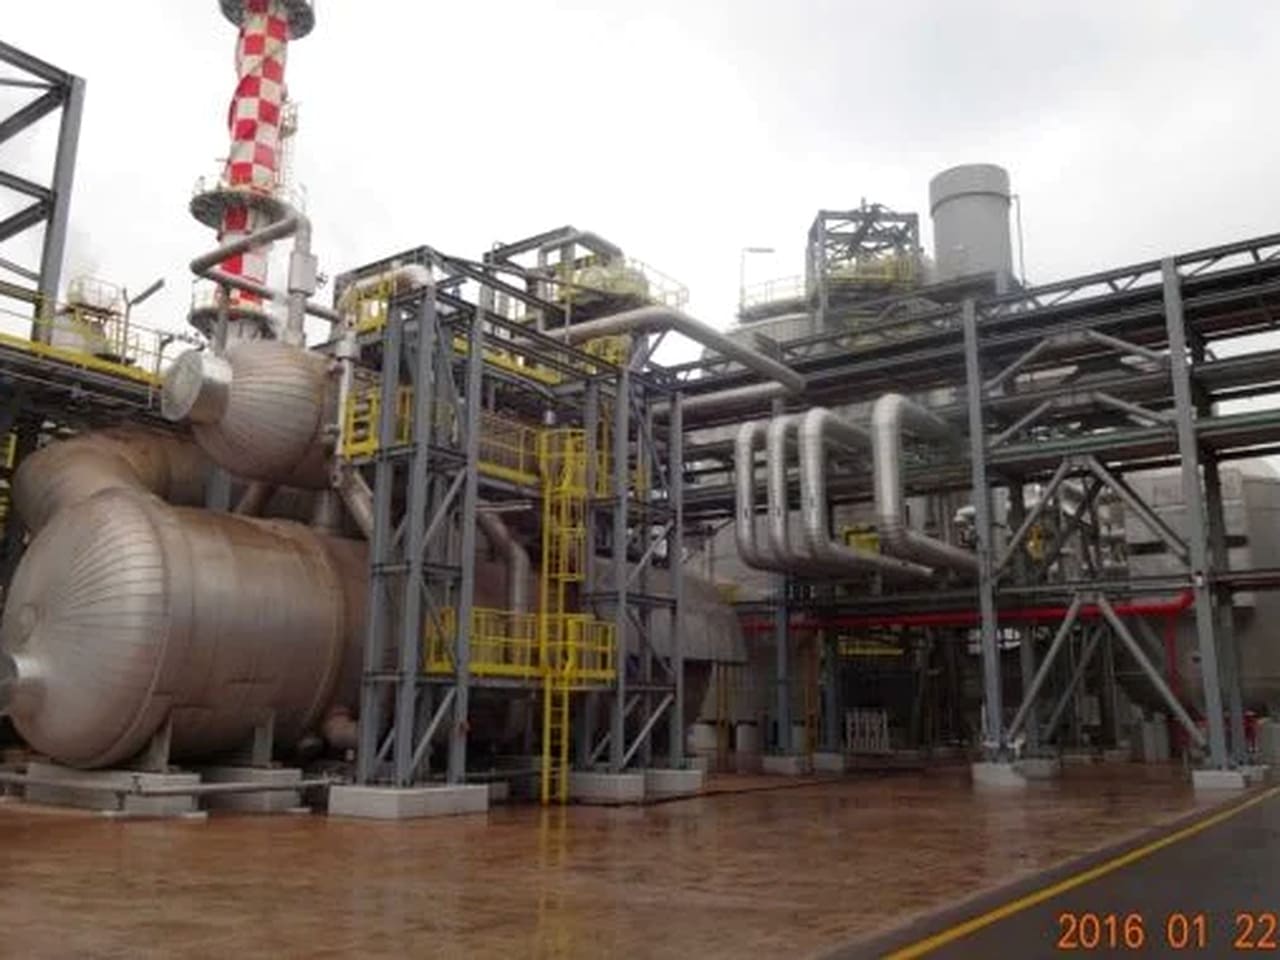
Waste Heat Boilers

Sulphur furnace boiler, fire-tube or water-tube

Industrial Heat Exchanger Piping Complex

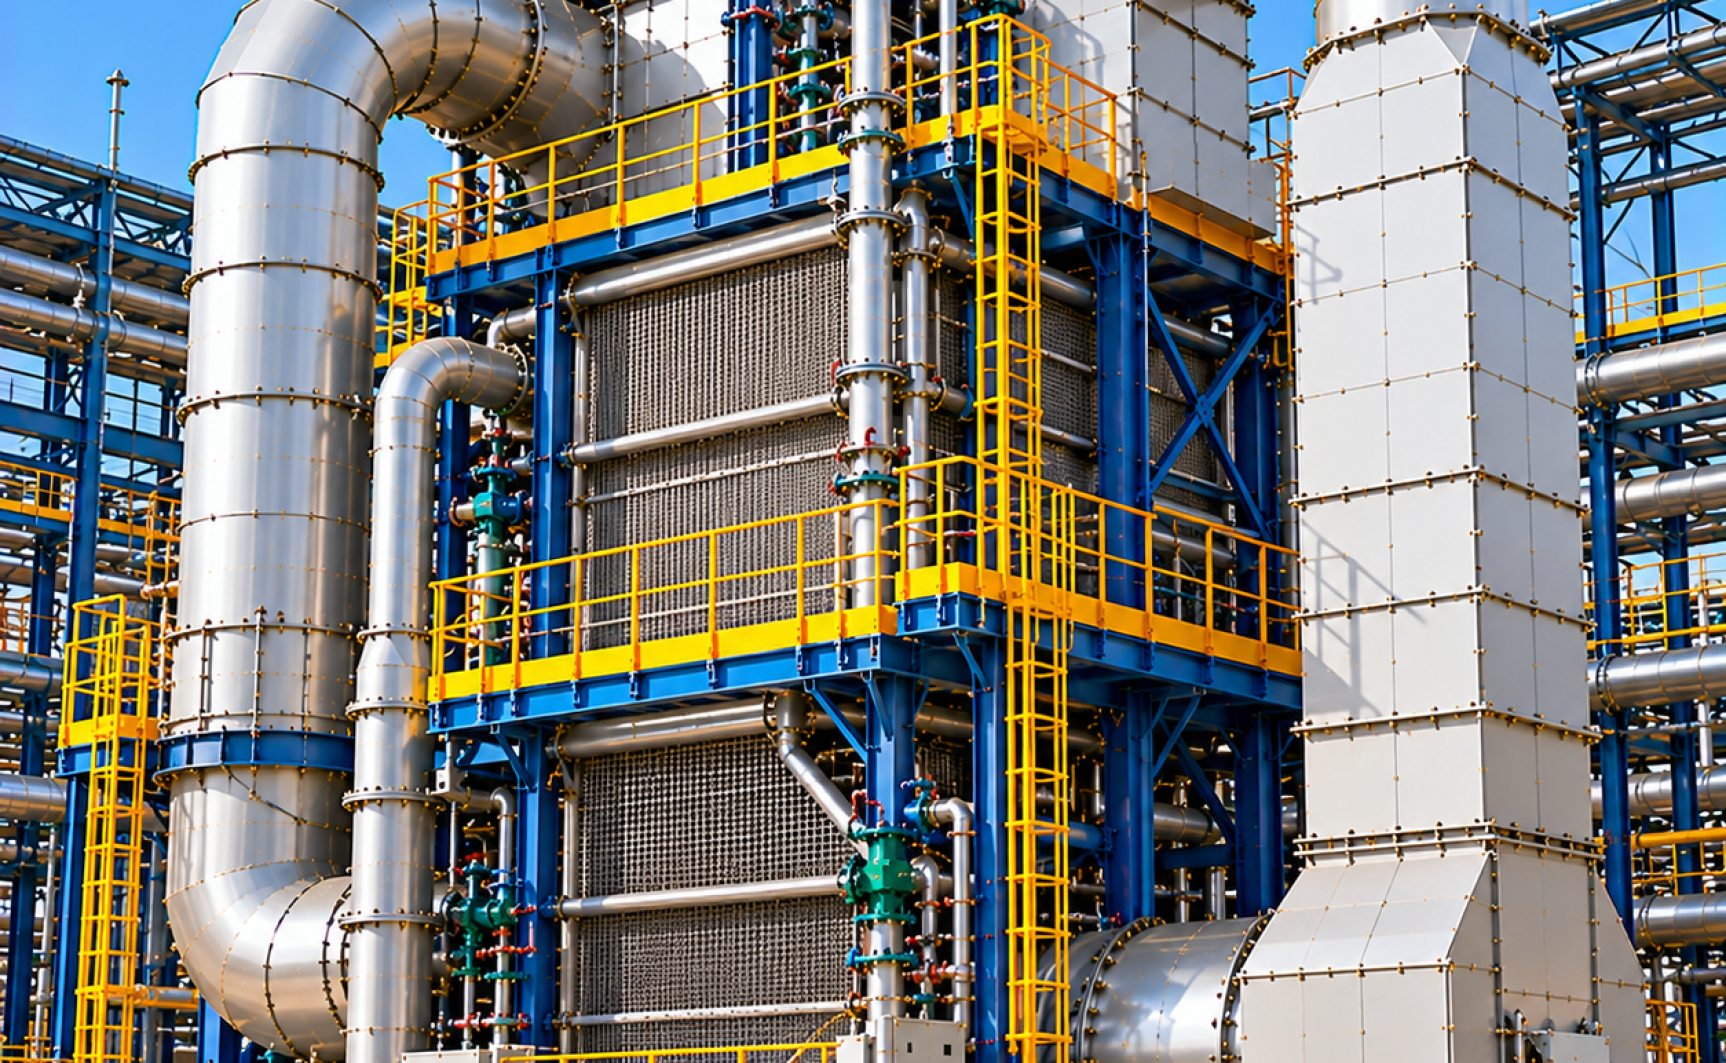
Gas Exchangers

Interpass exchangers between converter beds.

Industrial Heat Exchanger Under Blue Skies

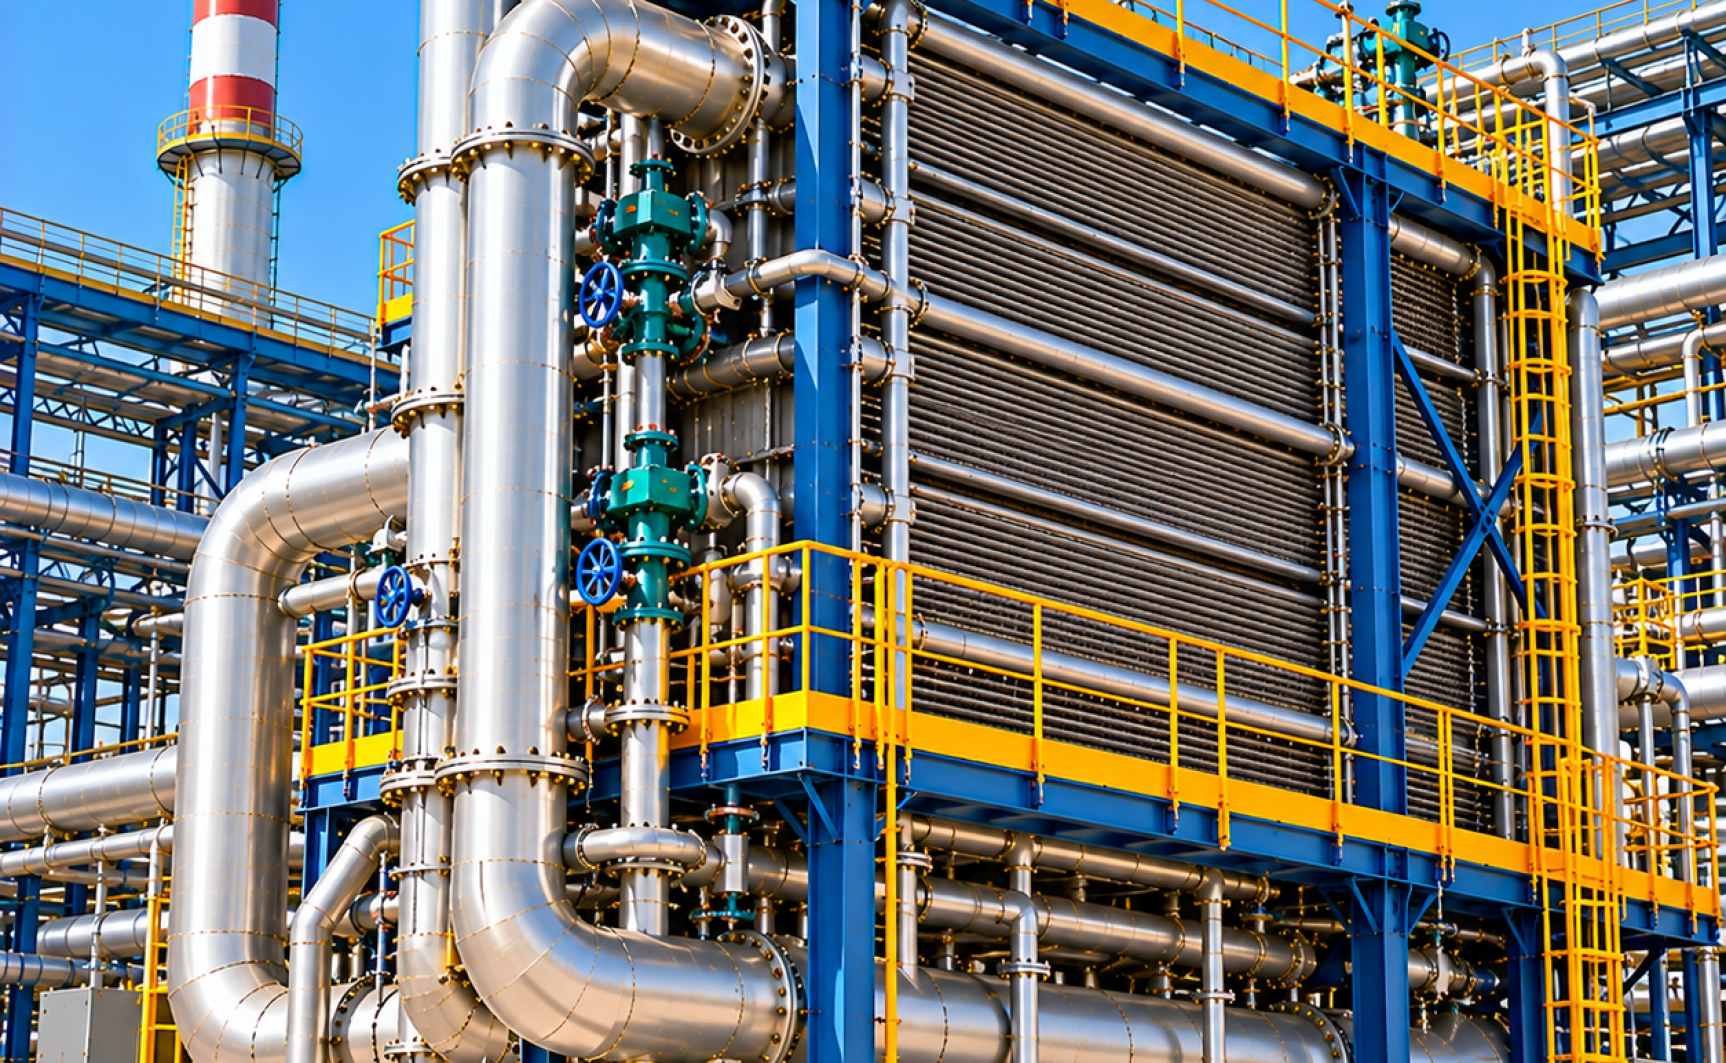
Preheaters

Air and gas preheaters for the plant.

Industrial Heat Exchanger Under Blue Skies (1)

Economisers (ECO)

Heats feed water to improve boiler efficiency.

Sunlit Industrial Heat Exchanger Complex (1)

Superheaters (SH)

 Steam temperature for the turbine or process.

Thermal Systems provides efficient Waste Heat Recovery Boilers for Sulphuric Acid plants

  • WHBs for 5500+ TPD Plant Capacity

  • Concept to Commissioning of SAP

  • Water tube boiler with provision for expansion

  • Fire Tube Boiler with external & integral gas bypass

  • Modular design for overseas shipment

Global Leaders with 250+ installations for Waste Heat Recovery Solutions in Sulphuric Acid Production application in various industries

Waste Heat Recovery Boiler

For Sulphuric Acid Plant (Sulphur Combustion Process)

In the sulphur-combustion route, molten sulphur is burned and the SO2 gas stream leaves the furnace at high temperature. The gas is cooled in a waste heat recovery boiler (WHRB), generating high-pressure steam and maximising energy recovery and acid yield.

Thermal Systems supplies fire tube boilers with external & integral gas bypass and water tube boilers with provision for future expansion — references up to 5,500+ TPD plant capacity.

DOWNLOAD BROCHURE

Waste Heat Recovery Boiler

For Sulphuric Acid Plant (Wet Sulphuric Acid Process)

In the WSA process, SO2 gas is produced at the operating temperature of the oxidation catalyst in the SO2 converter. Feeds containing sulphur are oxidised to SO2 by combustion and then cooled to the optimum catalytic conversion temperature in a waste heat boiler. The excess heat from this operation is recovered as steam. The catalytic conversion process reaction heat is recovered between the catalyst beds by superheating of steam.

TSPL supplies WHB | COOLERS | Super heaters for WSA plants

PREV

Nitric acid / weak nitric acid (WNA)

NEXT

Petcoke Calcination

Leave a Reply Cancel reply

Your email address will not be published. Required fields are marked *

Let's Convert Your Vision Into Reality

We support our clients throughout the entire project cycle – from identifying needs to commissioning, employing all our professional expertise in the most challenging contexts

Contact us

Get Social:

Linkedin

Quick Links

  • Home
  • About Us
  • Contact Us
  • Leadership
  • Capabilities

Explore Us

  • Industries
  • Applications
  • Products
  • Vendors
  • Policies

Address

  • Thermal Systems (Hyderabad) Pvt Ltd. Plot No.158, IDA Bollaram, Sangareddy, Hyderabad, Telangana, India
  • info@thermalindia.com

Get Social:

Linkedin

© 2026 Thermal Systems (Hyderabad) Pvt. Ltd. All Rights Reserved.

  • Privacy Policy
  • Terms & Conditions

Driven by passion. Grounded in purpose. Focused on results.

aerra@mail.com
+1 800 123 46 57
X-twitterFacebookInstagramLinkedin

Useful Links

  • Company
  • Services
  • Features
  • FAQs
  • Getting Started

Subscribe

Our expertise, as well as our passion for web design, sets us apart from other agencies.

© 2026 Aerra byWebGeniusLab. All Rights Reserved