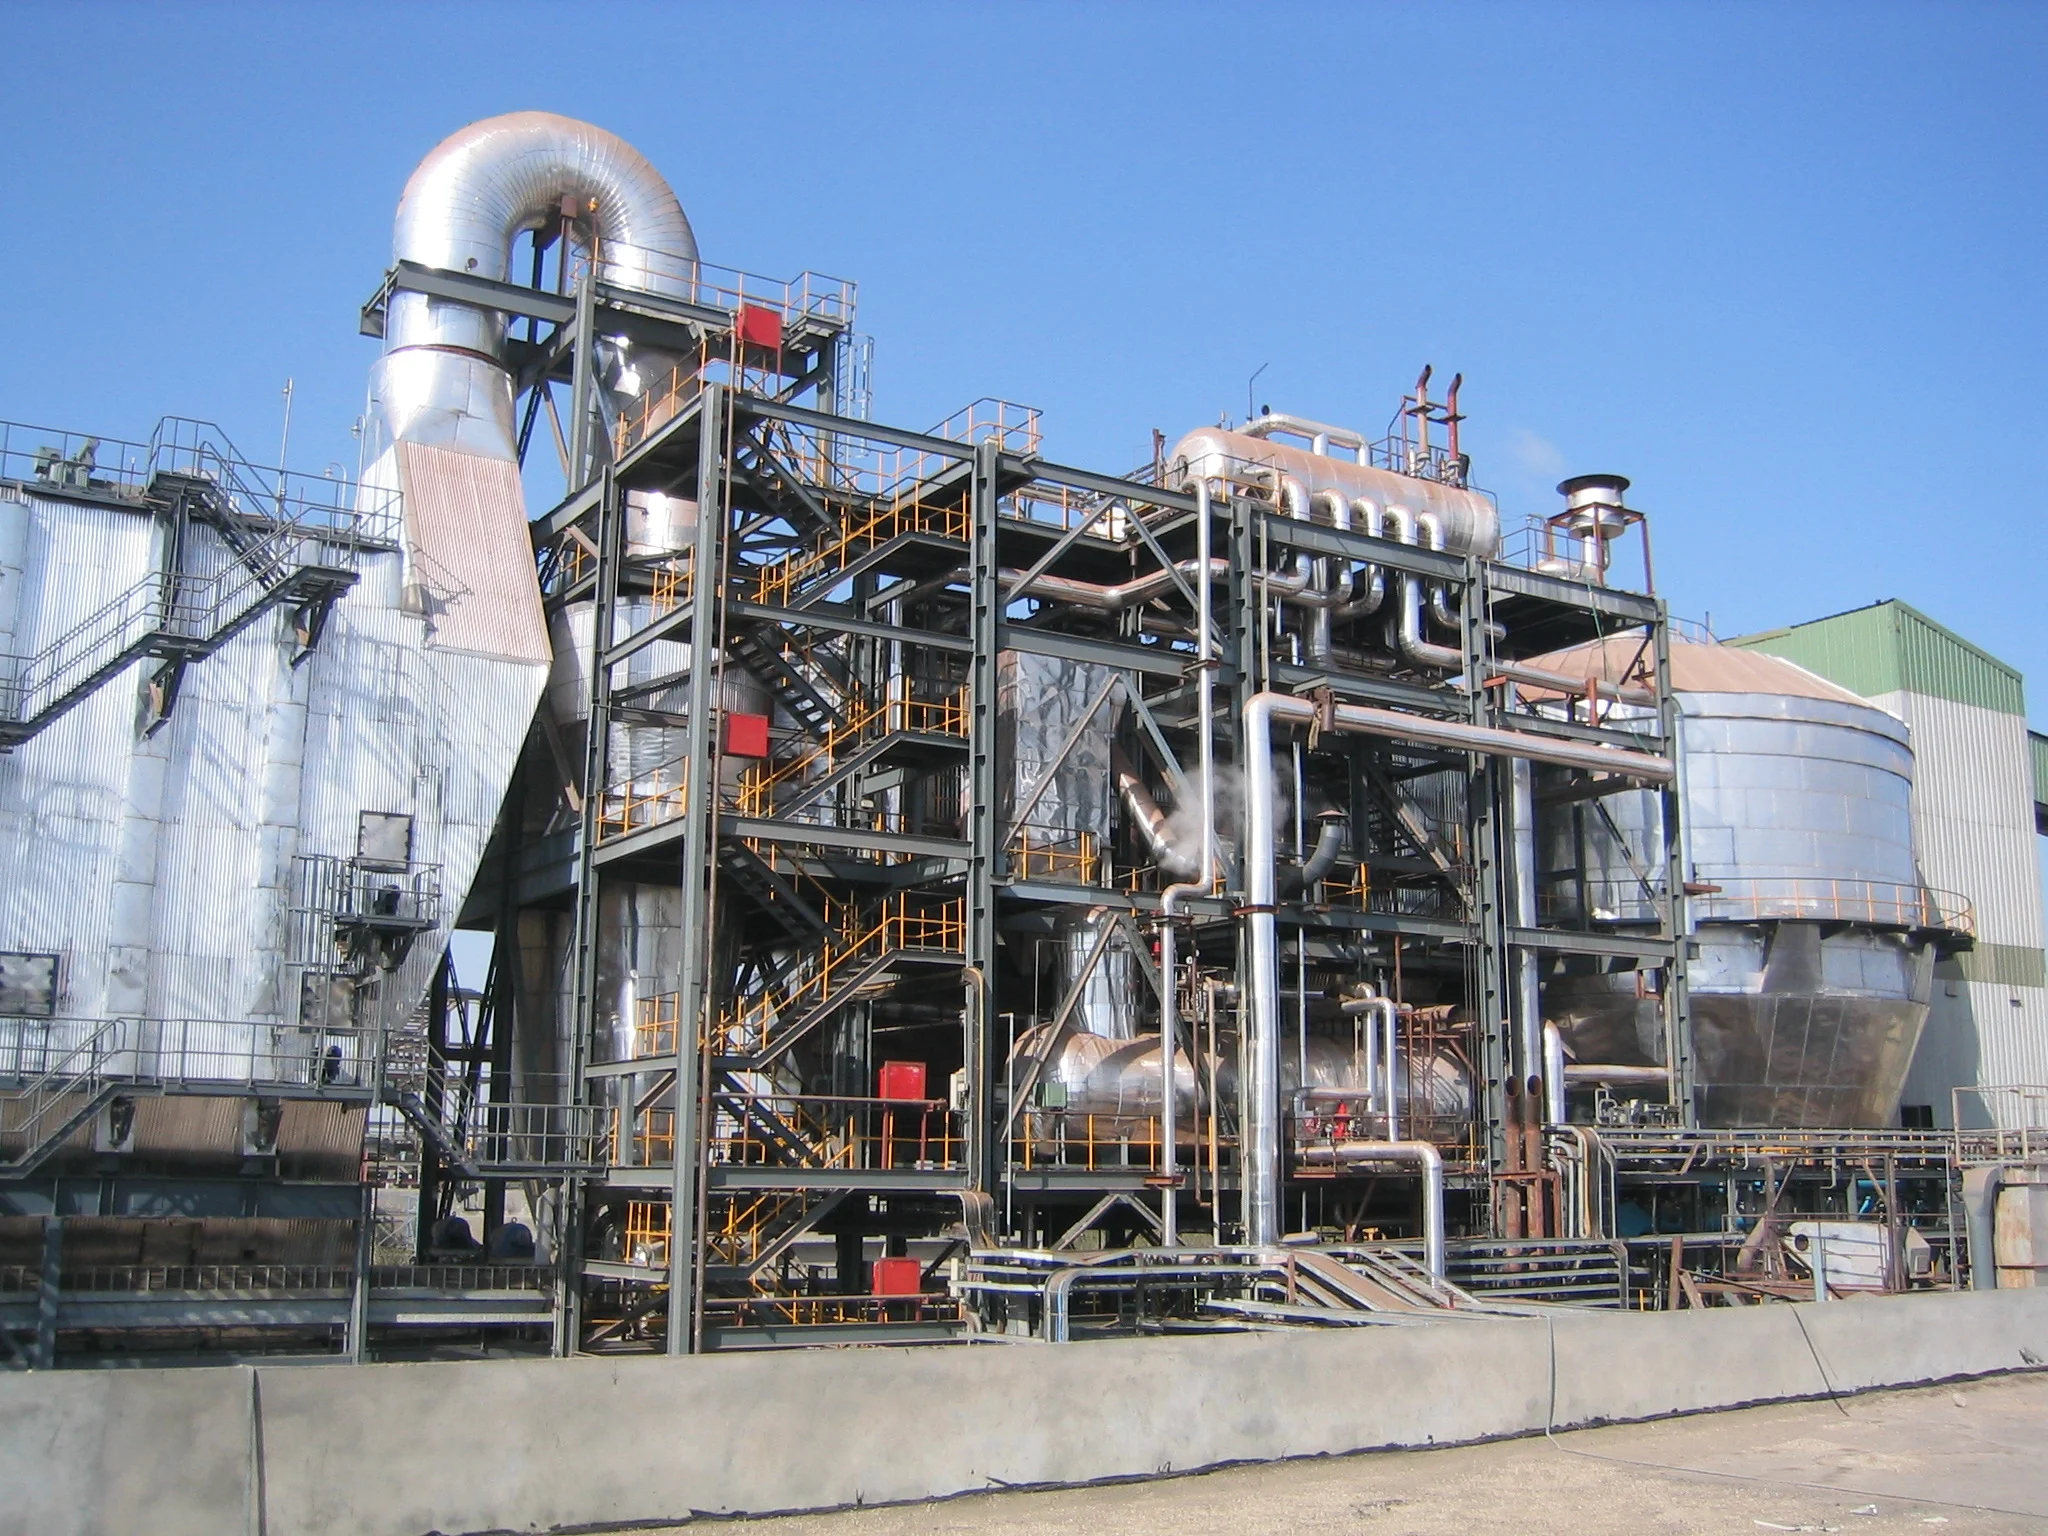
Water Tube Design for Various Applications
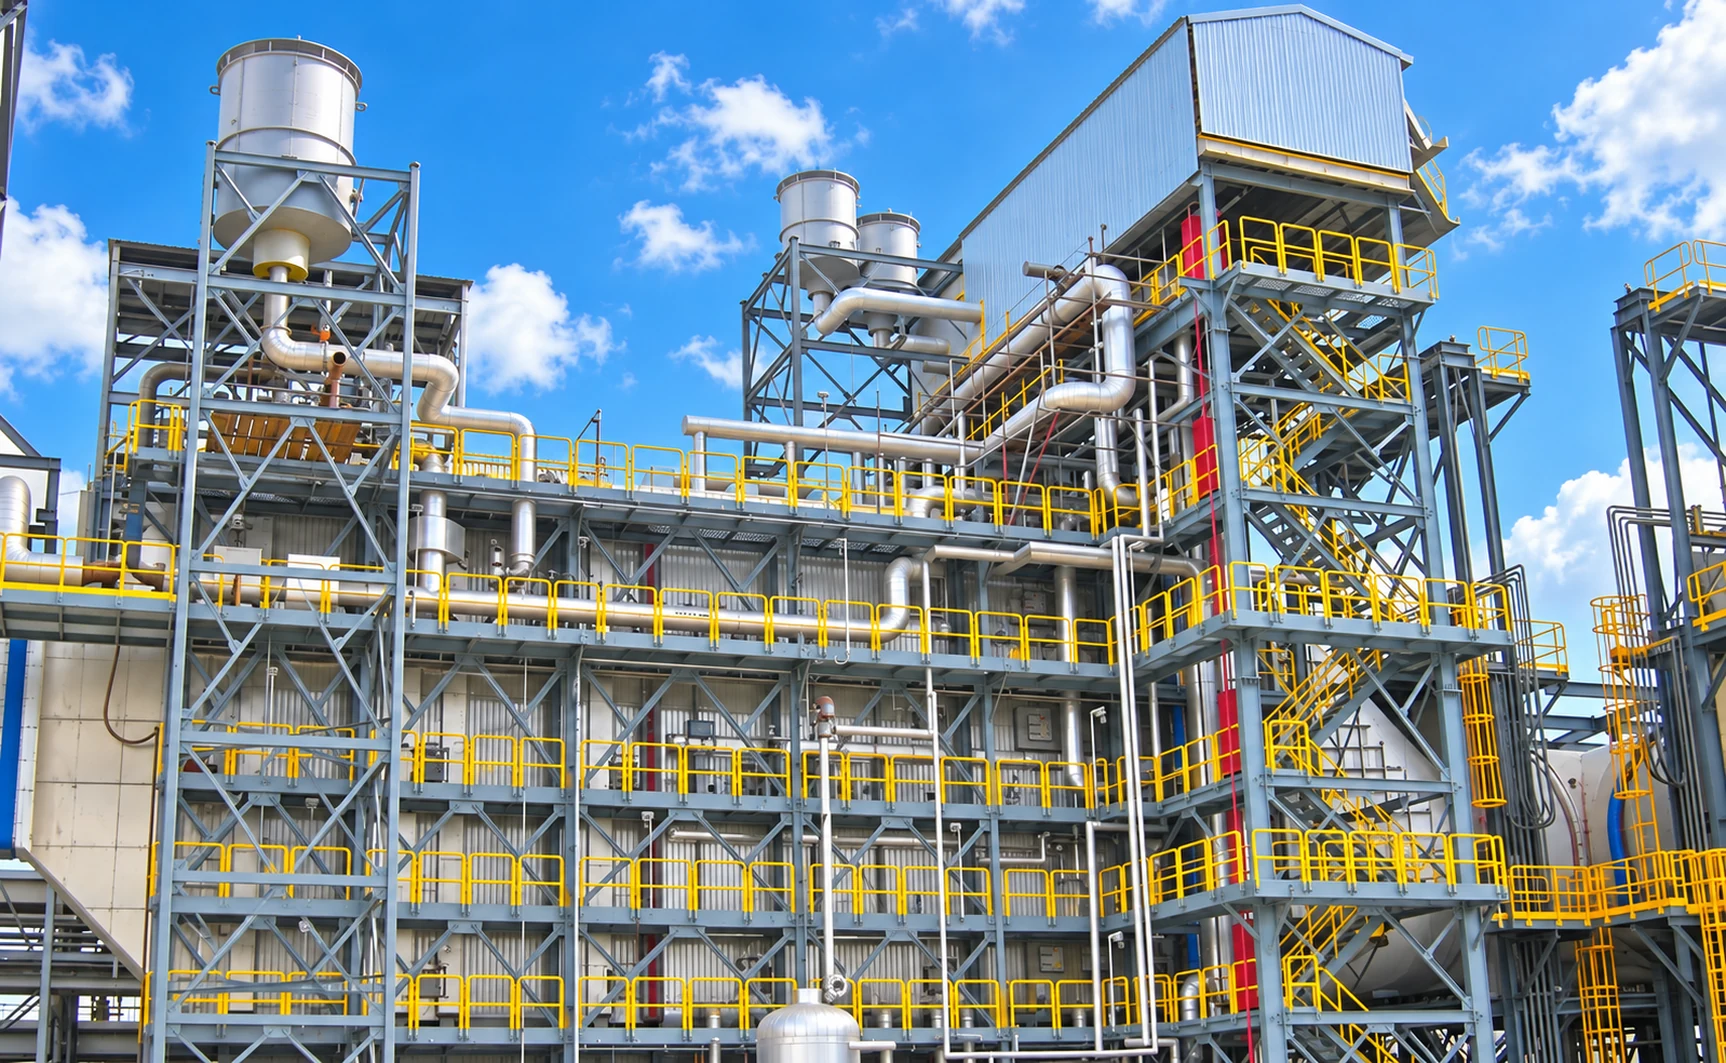
Fire tube or water tube, our waste heat recovery boilers take hot process gas and turn it into steam for power or process. More than 550 of them are in service worldwide.
128 TPH
Largest unit capacity
68 kg/cm²
Steam pressure
284 °C
Steam temperature
27
Installations in hydrogen units
What it is
- Fire Tube design with(out) Hot / Cold Bypass
- Design consideration for high gas side operating pressure
- Single piece / extended ferrules
- Special consideration for Metal dusting issues
- GAPFREE WELDING to avoid CREVICE CORROSION
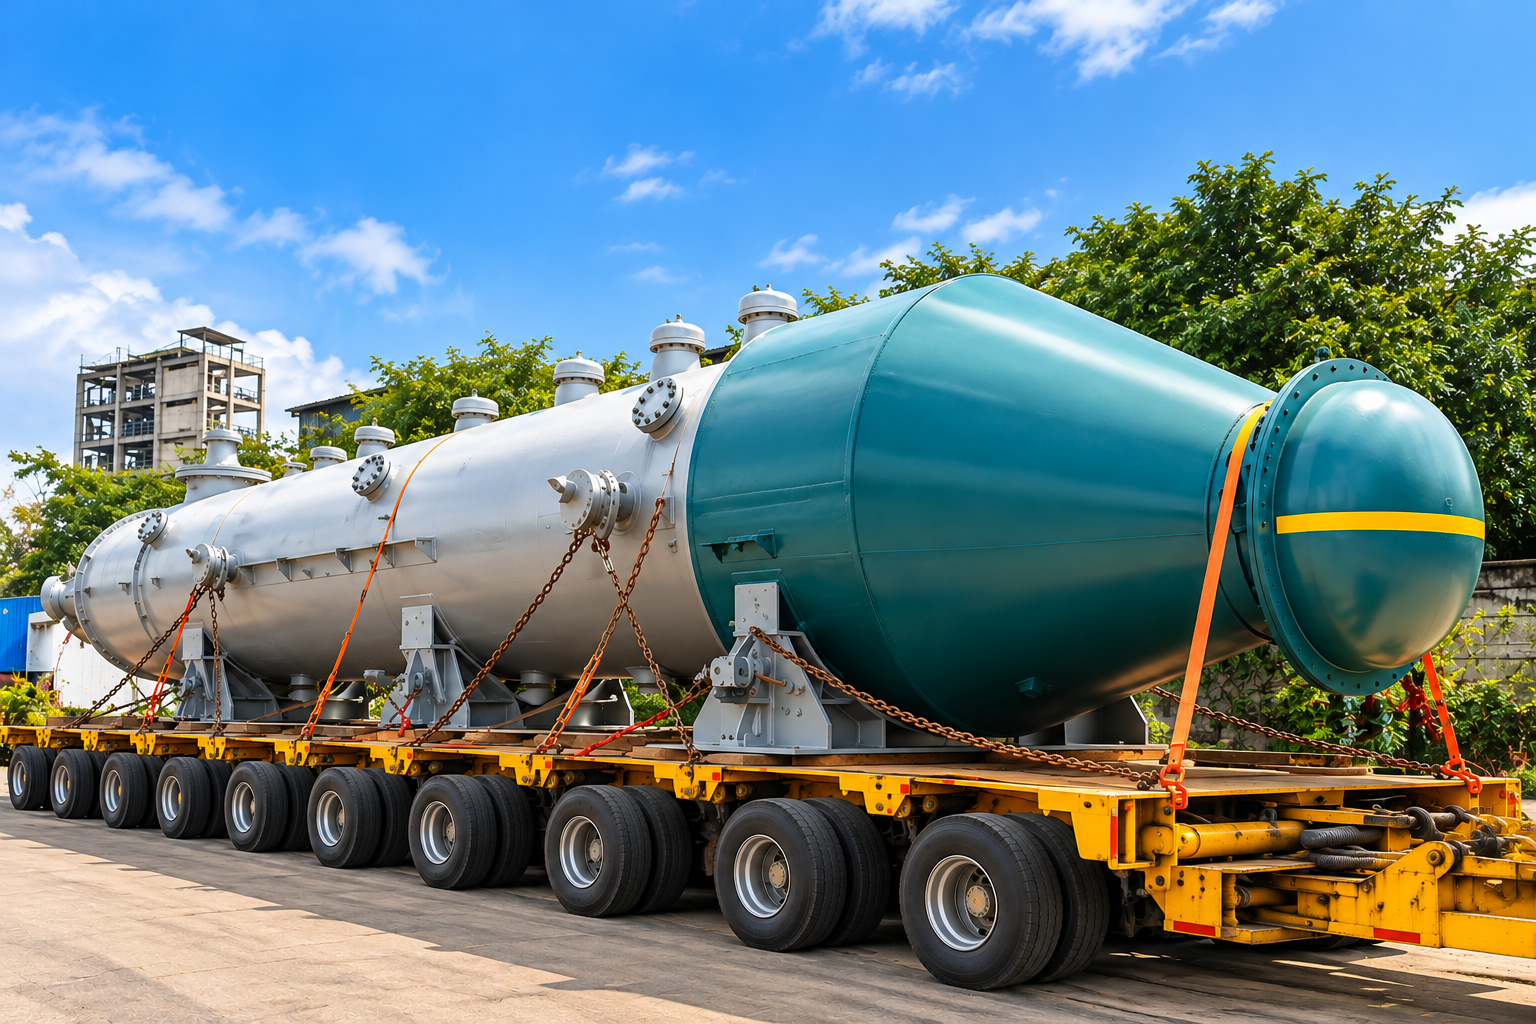

Water tube waste heat boilers
How we build it
- Fire tube: refractory inlet channel, ferrules, gap-free tube-to-tubesheet welding, gas bypass, integral or elevated drum
- Water tube: vertical or horizontal, natural or forced circulation, inline or offset to suit the plant
- Online cleaning: rapping, hammering, soot blowing to suit the dust
- Modular construction for transport and site assembly; overseas shipment to over 40 countries
- Designed and manufactured in-house under ASME S and U stamps, IBR and PED
Incinerator (SRU)
For sulphuric acid plants, Thermal Systems supplies water tube waste heat boilers with provision for future capacity expansion, steam-flooded air heaters and custom gas–gas heat exchangers.
These cover the sulphur-burning, metallurgical off-gas and spent-acid routes, up to 5,500+ TPD.
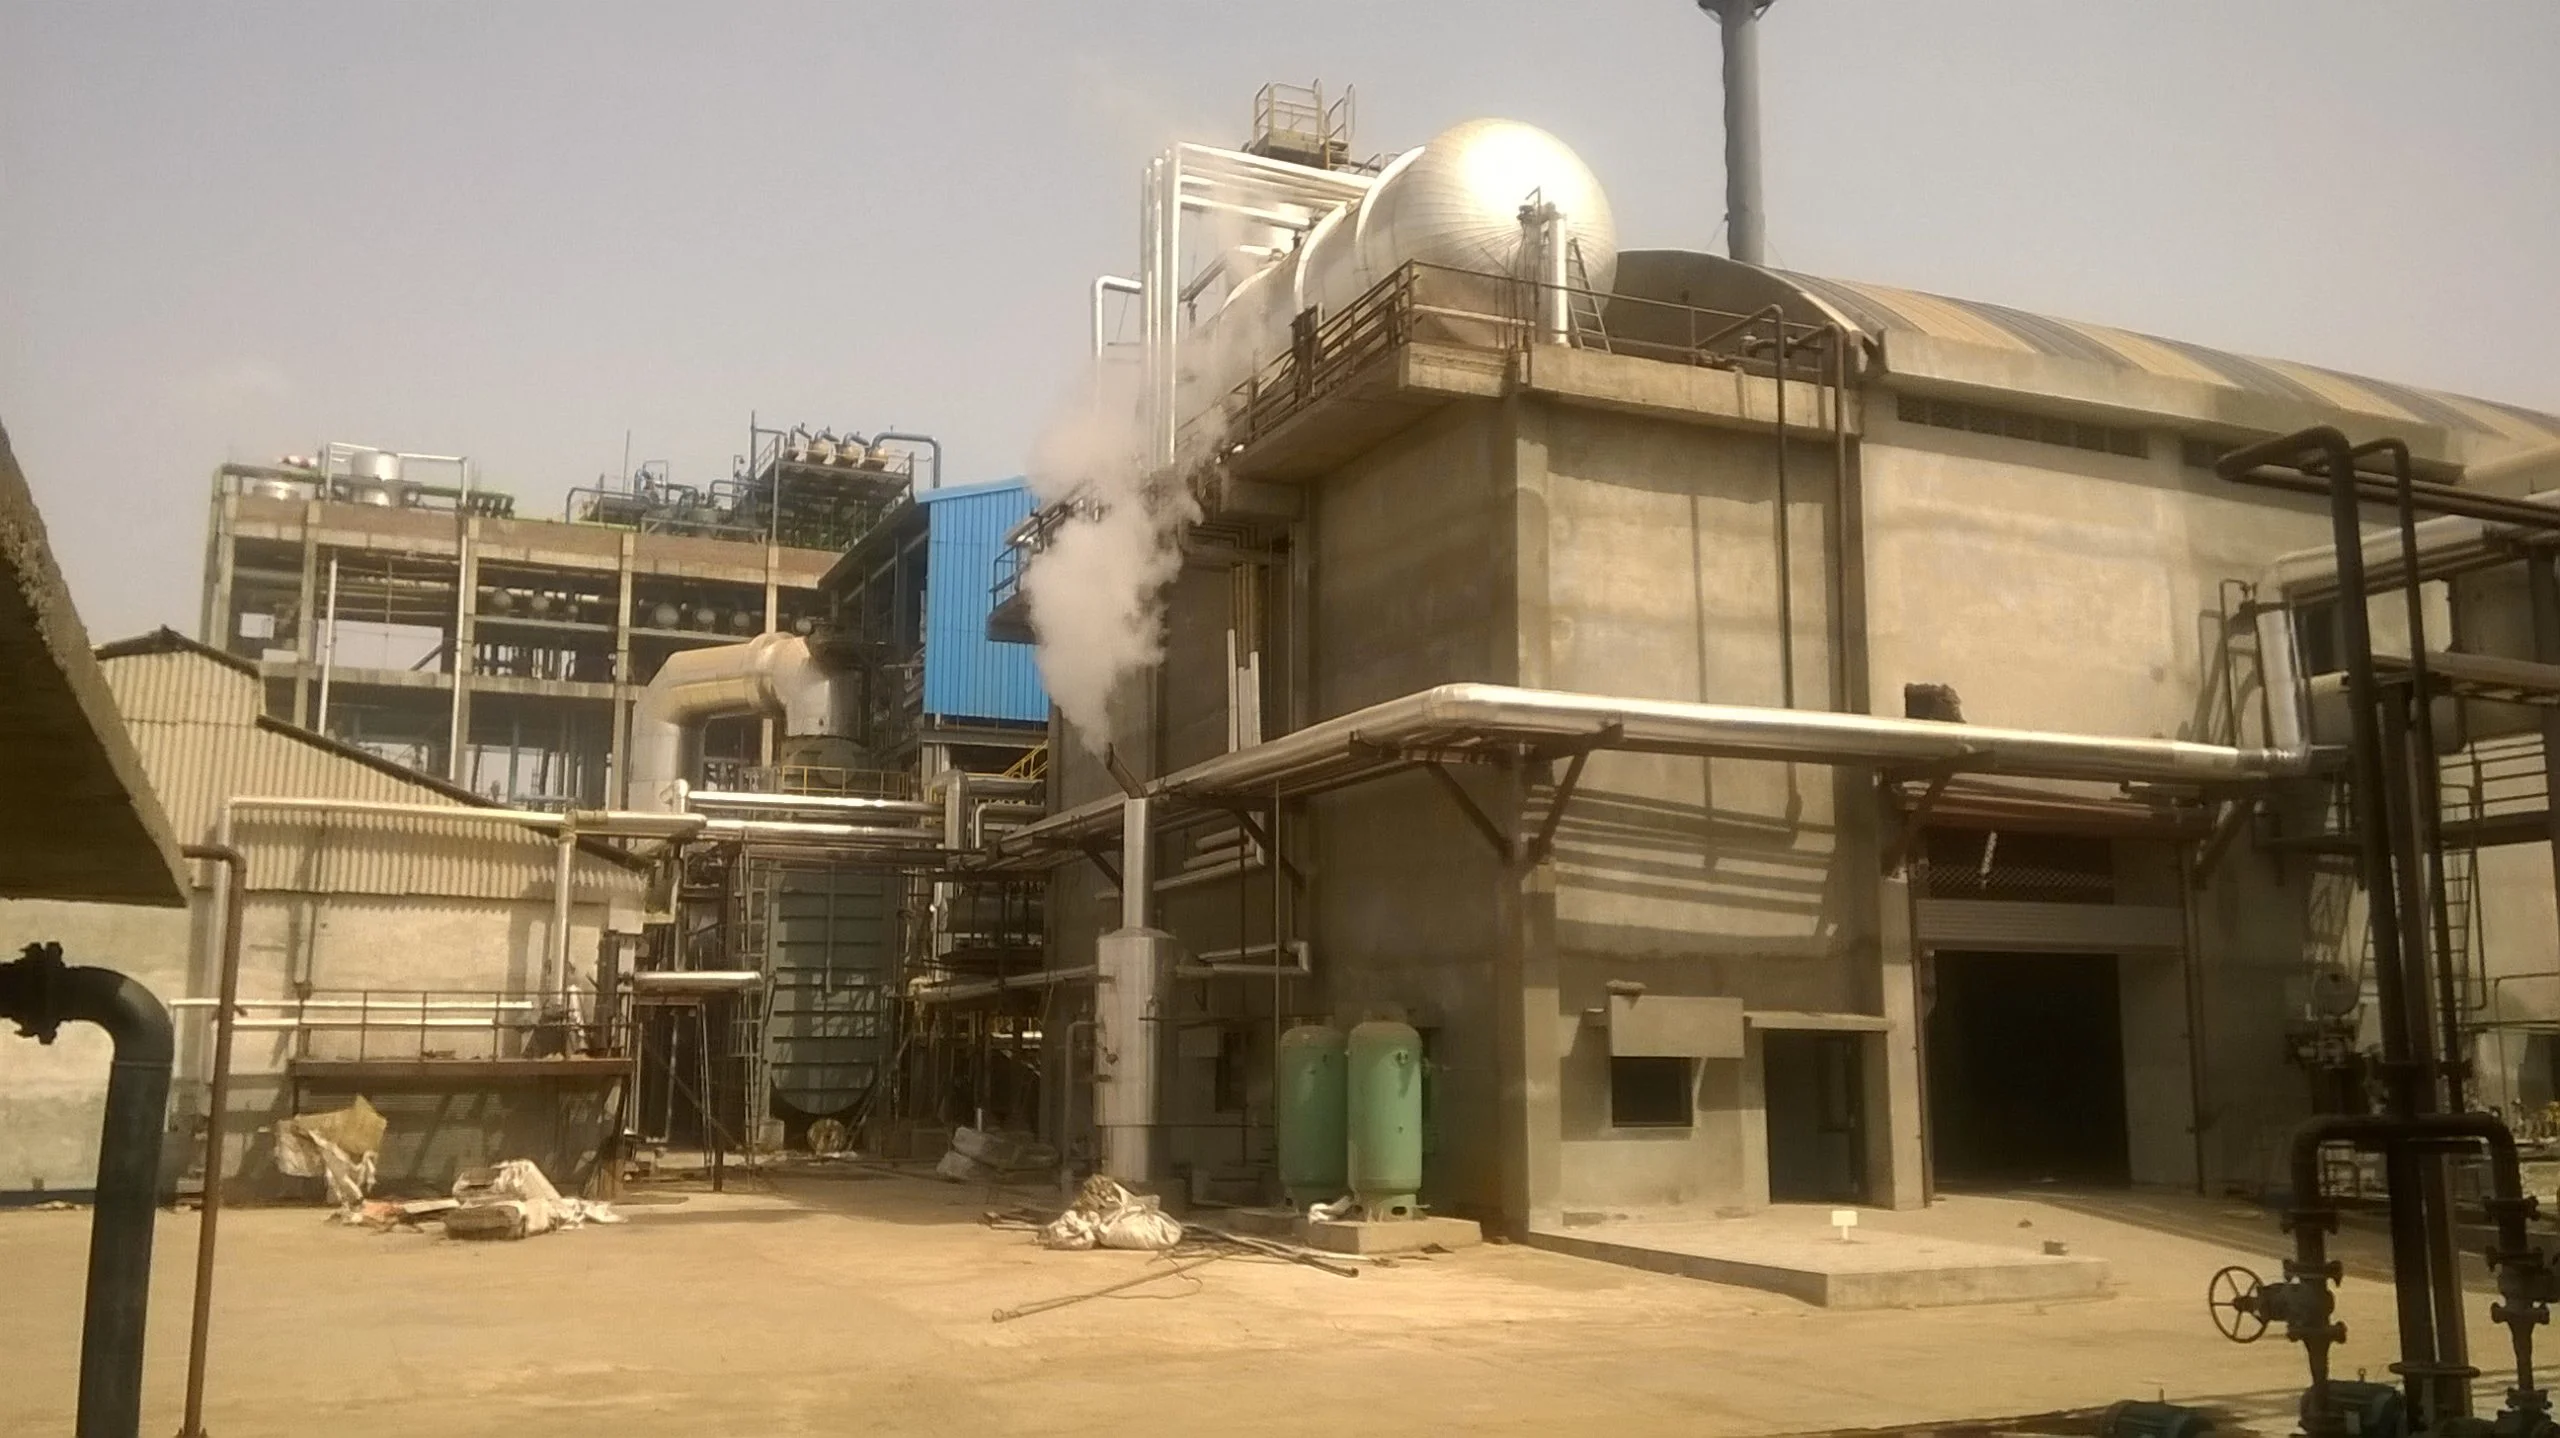
Tail Gas Treatment Unit (TGTU)
In tail gas treatment units, the treated gas stream is incinerated and its heat recovered in a waste heat boiler cum superheater.
Thermal Systems has supplied TGTU packages including 2 × 100 TPD TGTU boilers at HPCL Mumbai.

Sulphuric Acid Plant
Spent sulphuric acid is thermally decomposed in the regeneration furnace, generating high-temperature gas that is recovered in a waste heat boiler producing high-pressure steam.
Thermal Systems supplies fire tube waste heat recovery boilers (WHRB) for SARU service, including the world’s largest operating installation on a 1,000 TPD SARU.
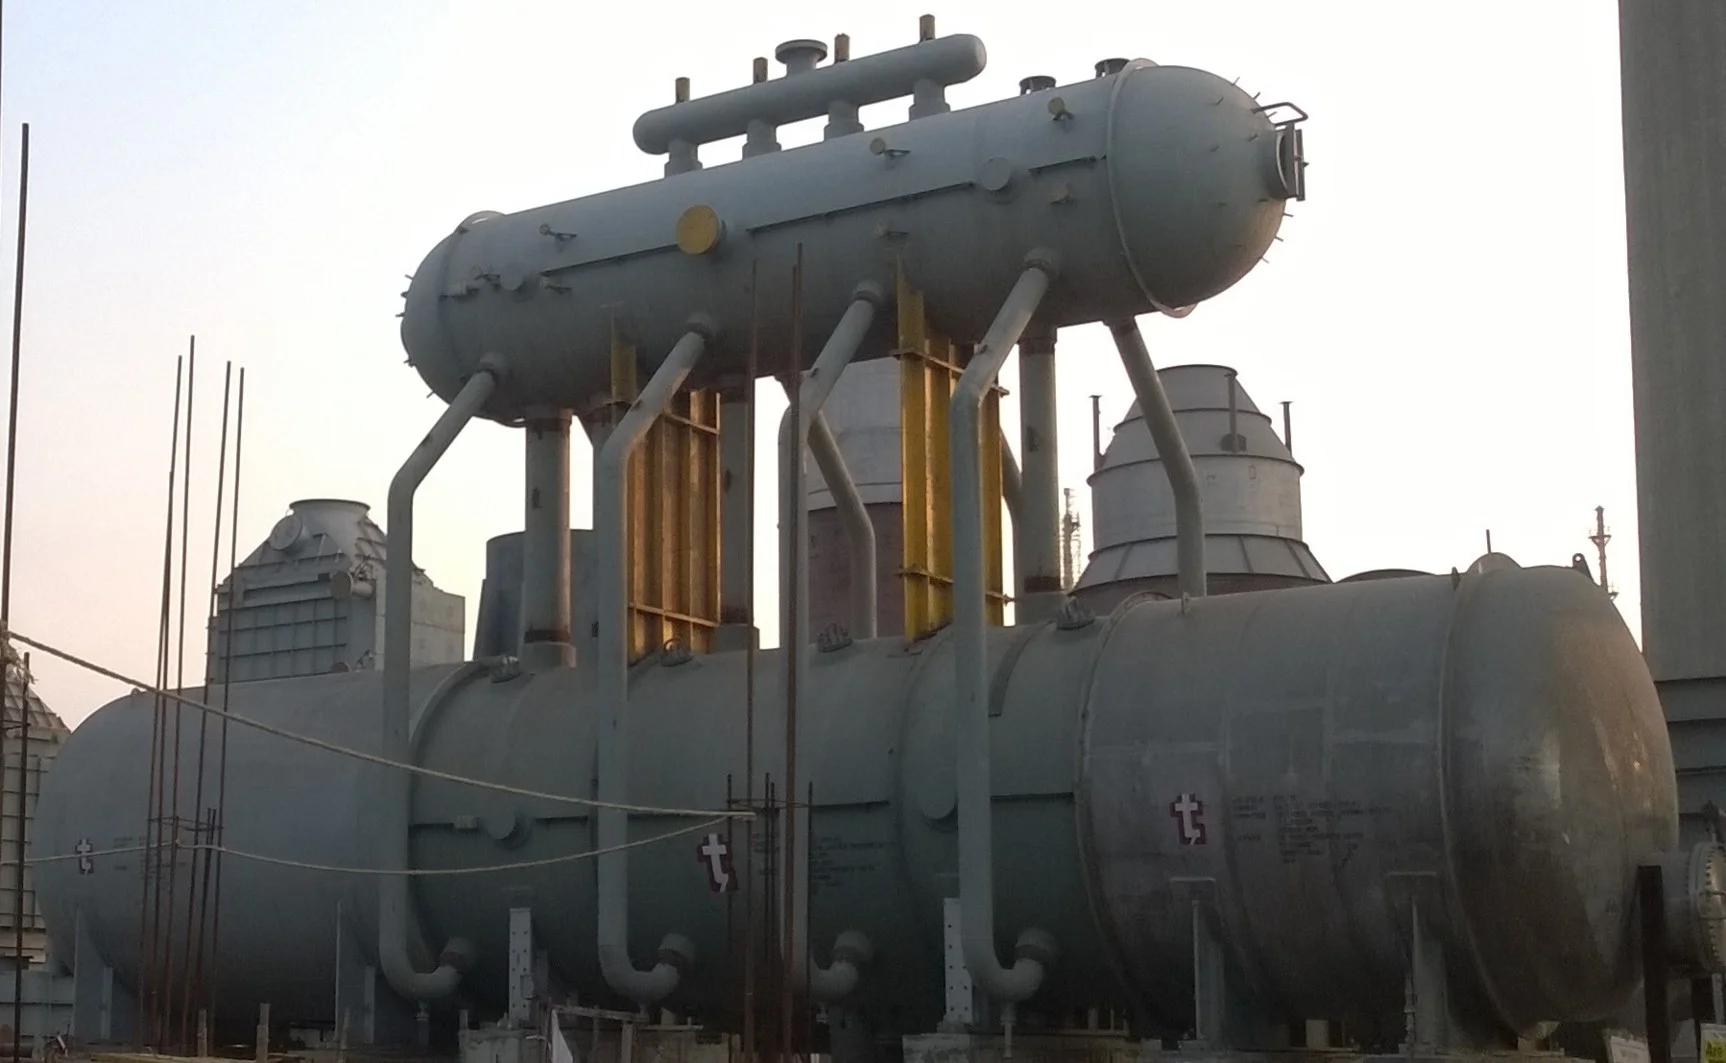
Petcoke Calcination
Calciner exhaust gas — high-temperature, dust-laden, with fluctuating flow — is recovered in vertical, 2-pass, natural-circulation, single-drum water tube boilers with membrane-wall first pass, proven in India and overseas.

Coke Oven Batteries
Waste flue gas from by-product and non-recovery coke oven batteries is recovered in WHRBs generating HP steam for power.
Inline and offset configurations suit the battery layout, with references including India’s largest installation of 8 × 57 TPH boilers on a single non-recovery coke oven plant.

DRI Kilns
Hot, dust-laden kiln exhaust from sponge-iron rotary kilns is recovered in vertical/horizontal water tube WHRBs — natural and forced circulation, inline and offset arrangements, with proven cleaning systems.
References include India’s largest WHB for a 1,250 TPD DRI kiln.
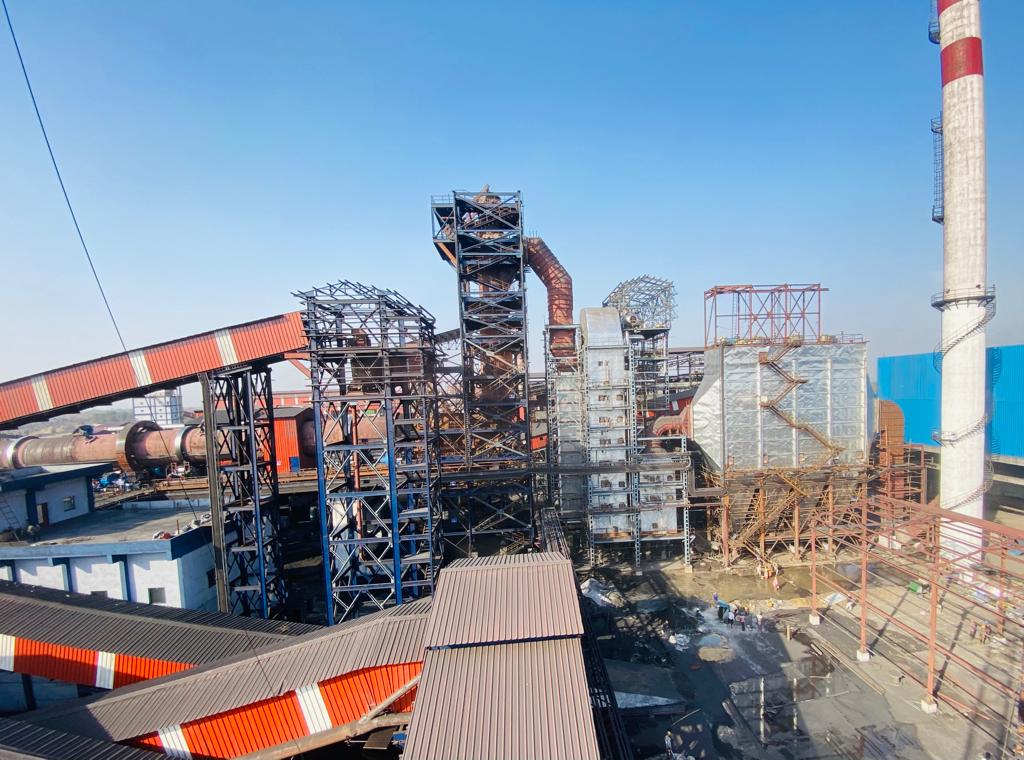
Copper Smelter
For copper smelters, Thermal Systems supplies waste heat recovery boilers (WHRB) on smelter and converter off-gases — 3 Pass Uptake–Downtake–Convection design with water-cooled ducts and online rapping.
For the acid plant section, Thermal Systems supplies gas–gas heat exchangers and pre-heating units, shop- or site-assembled.

Zinc Roaster
Zinc concentrate is roasted at about 950–1,000 °C, producing high-dust off-gas that is cooled in a roaster waste heat recovery boiler ahead of the sulphuric acid plant.
Thermal Systems’ boilers feature 3 Pass Uptake–Downtake–Convection design, water-cooled horizontal ducts and online hammering/rapping systems proven on high-dust service.