Destroy the gas, keep the heat.

128 TPH
Largest unit capacity
68 kg/cm²
Steam pressure
284 °C
Steam temperature
27
Installations in hydrogen units
What it is
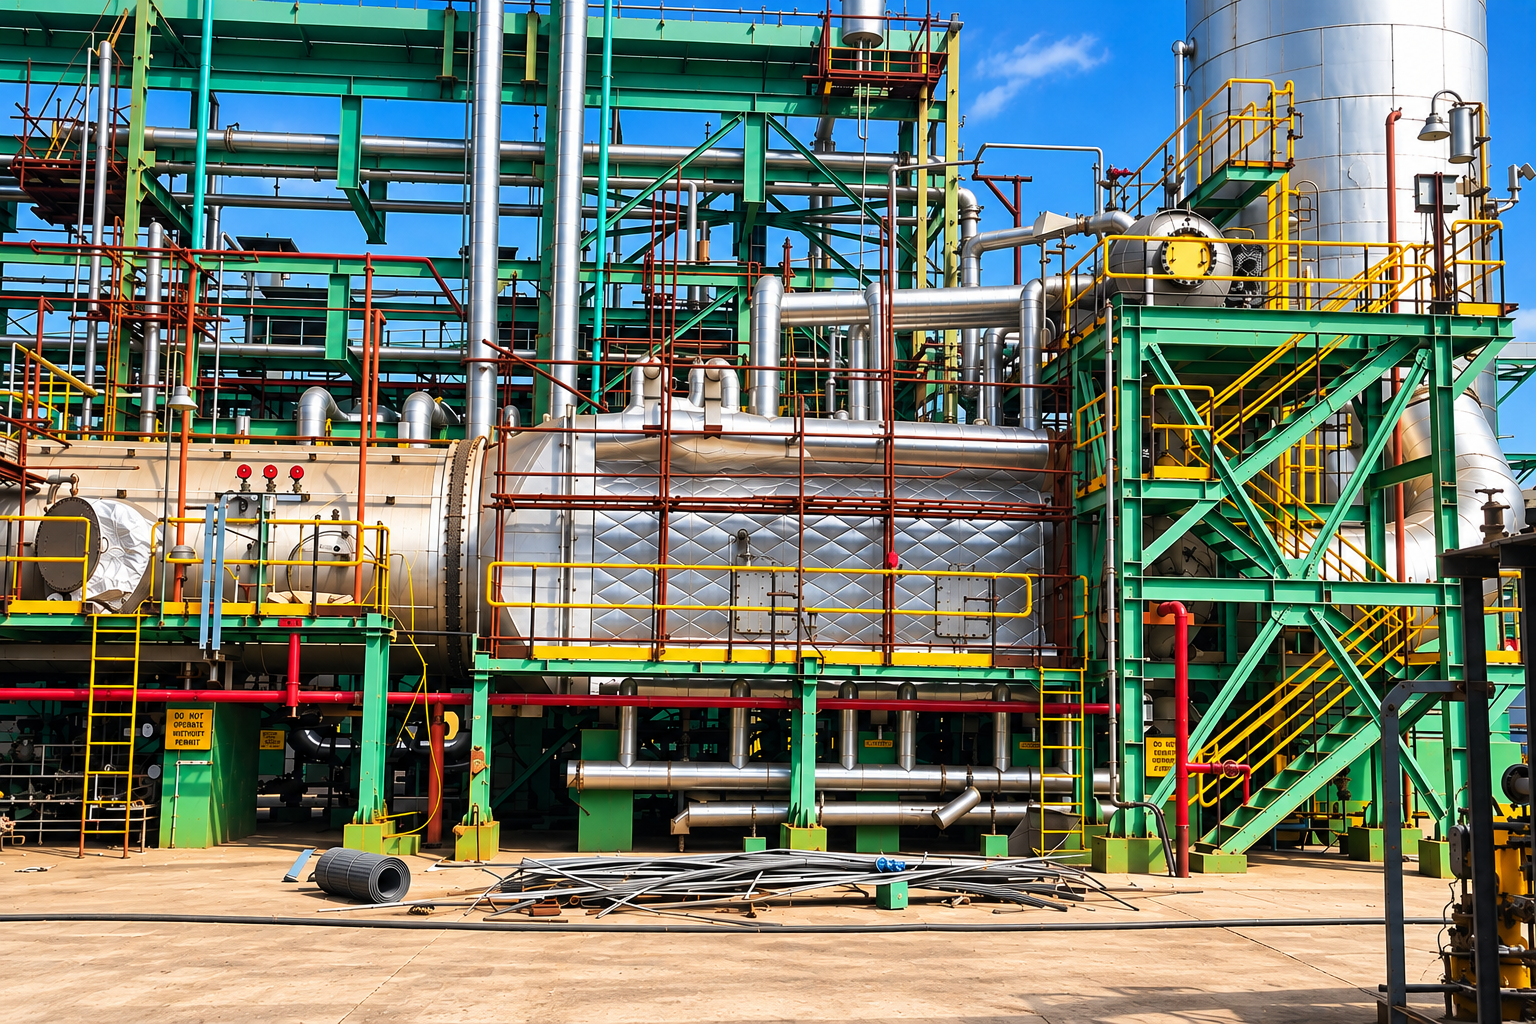
The tail gas of a sulphur recovery unit, and the liquid and gaseous wastes of chemical, pharmaceutical and petrochemical plants, are destroyed in a refractory-lined incinerator chamber with an auxiliary burner, at a temperature and residence time that the regulations define. The heat released is recovered in a waste heat boiler behind the chamber and raised to turbine or process conditions in a superheater. We engineer the chamber, the burner interface, the boiler and the superheater as one system, so that destruction temperature, residence time and steam output are designed together.
- Fire Tube / Water Tube construction of WHB
- Modular construction for ease of site assembly Reaction
- Furnace (MCC) package for SRU
- Incinerator Package for SRU

How we build it
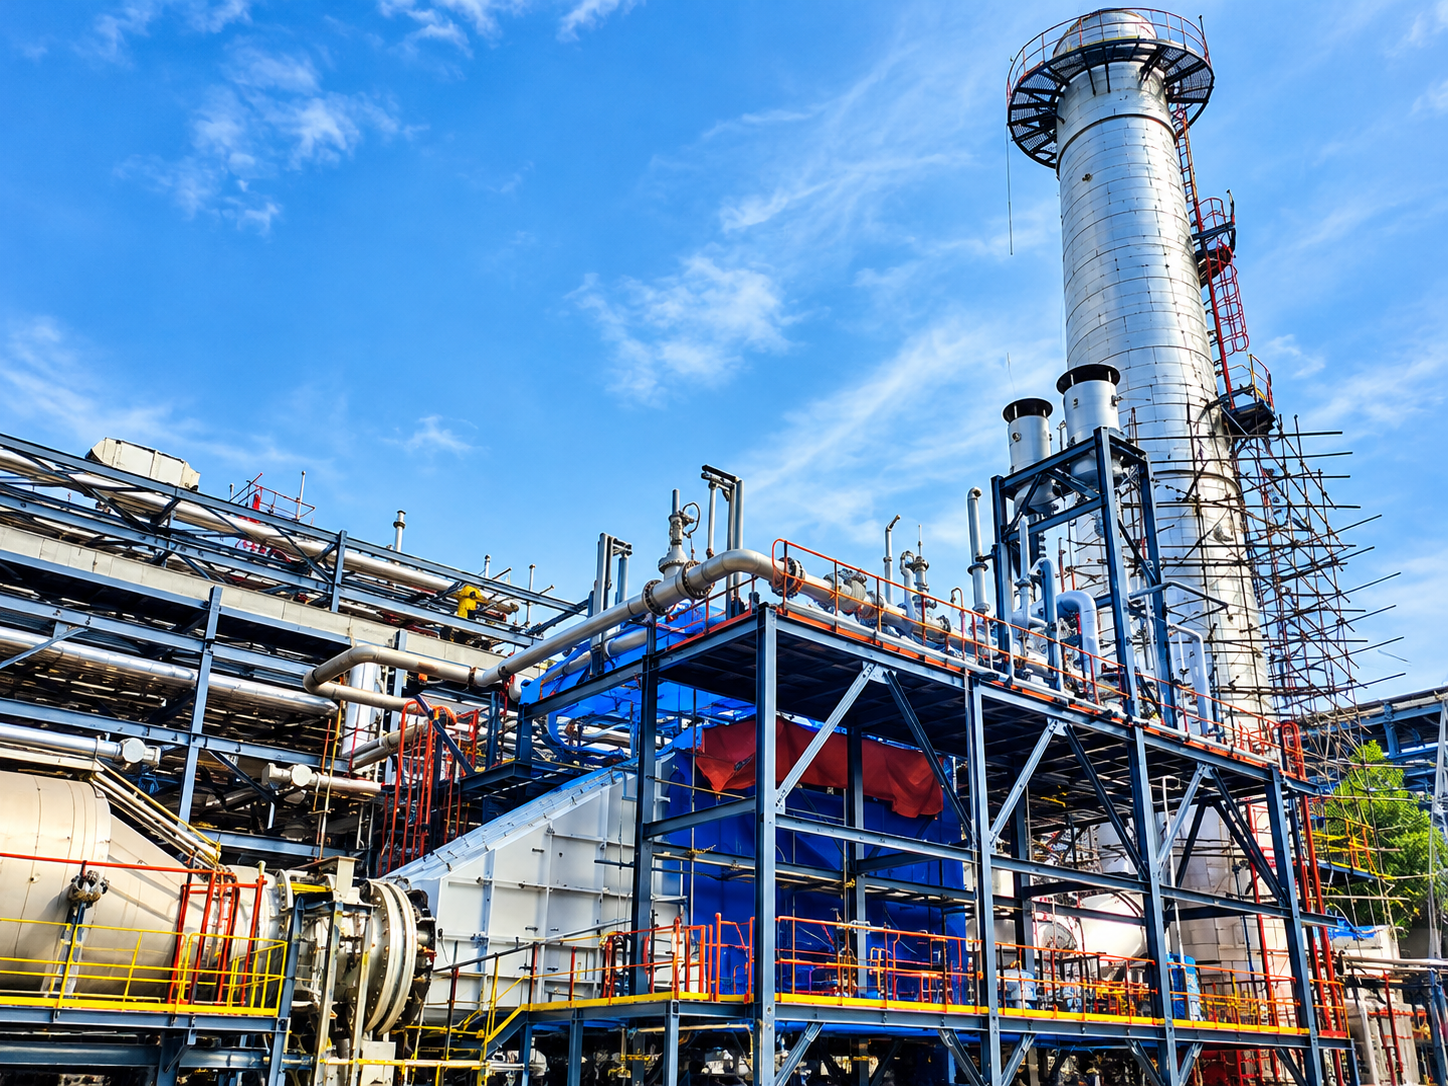
- Refractory-lined incinerator chamber with burner interface and auxiliary fuel
- Waste heat boiler in fire-tube or water-tube construction, designed with the chamber for the required residence time
- Superheater for turbine or process steam conditions
- Tube metals and temperatures chosen for sulphur and chloride-bearing gas
- Open, cleanable gas path for salt and ash deposits
- Modular construction for site assembly; built under ASME U and S stamps


For Sulphur Recovery Unit
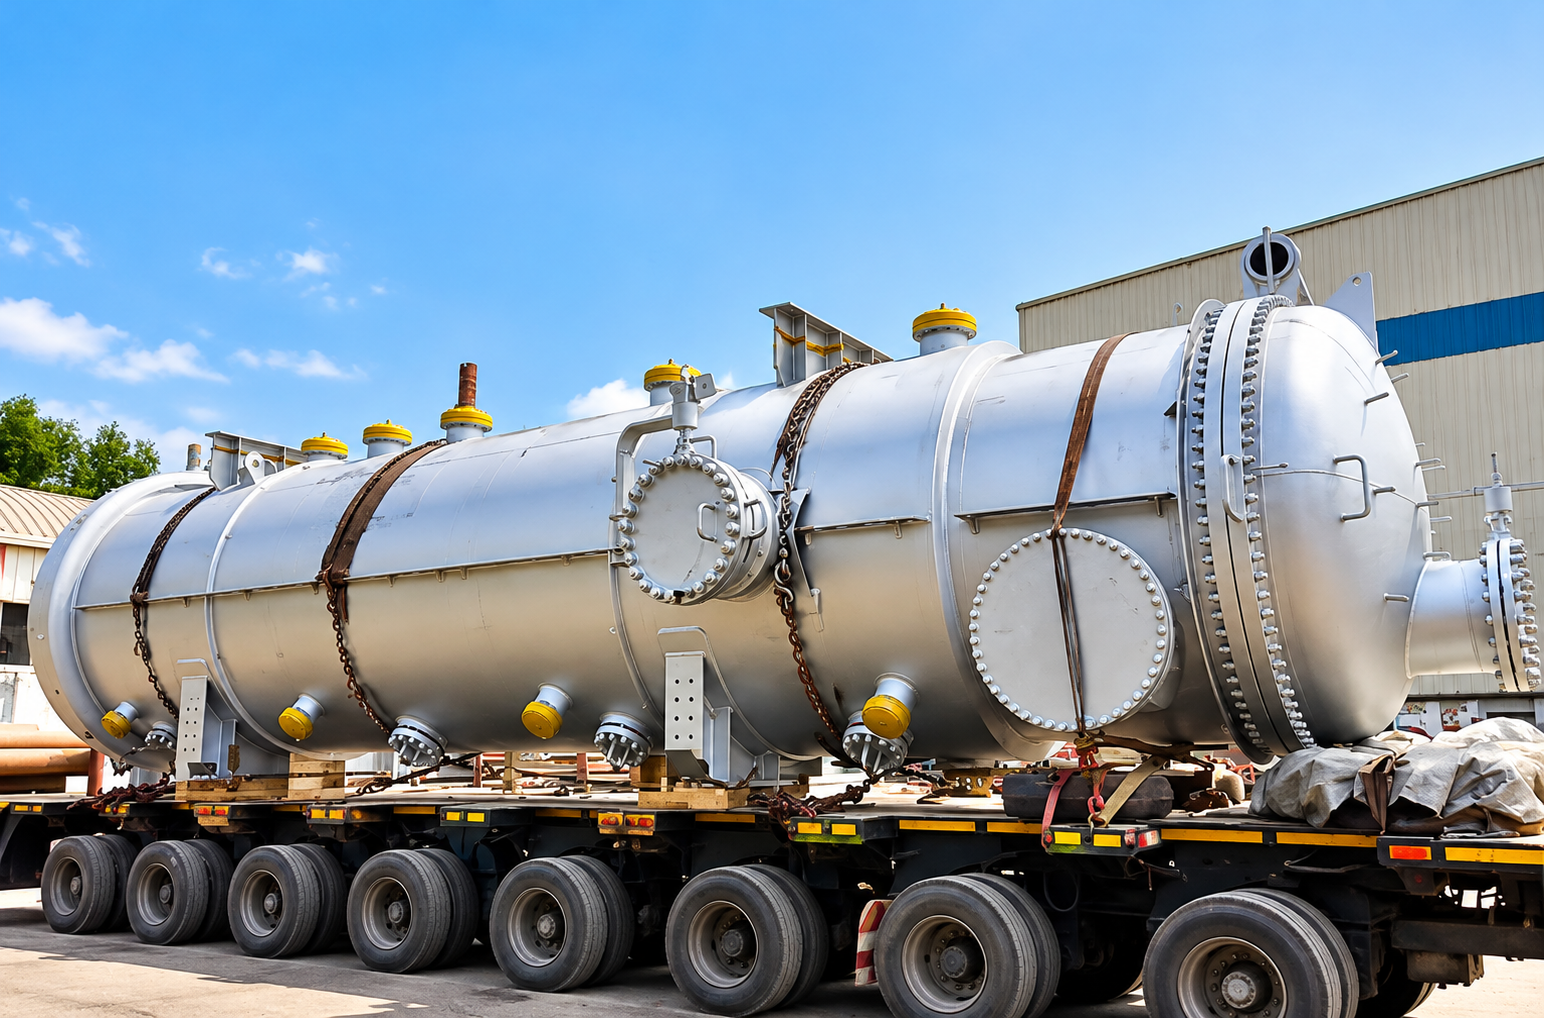
In the Claus process, H2S-rich acid gas is burned in the reaction furnace, generating gas at around 1,300 °C. The furnace outlet gas is quenched in the MCC waste heat boiler, generating HP/MP steam.
Thermal Systems supplies complete Reaction Furnace (MCC) packages — burner, chamber, boiler and EBOP — in fire tube construction, with superheaters suitable for internal and import steam.

For Sulphur Recovery Unit
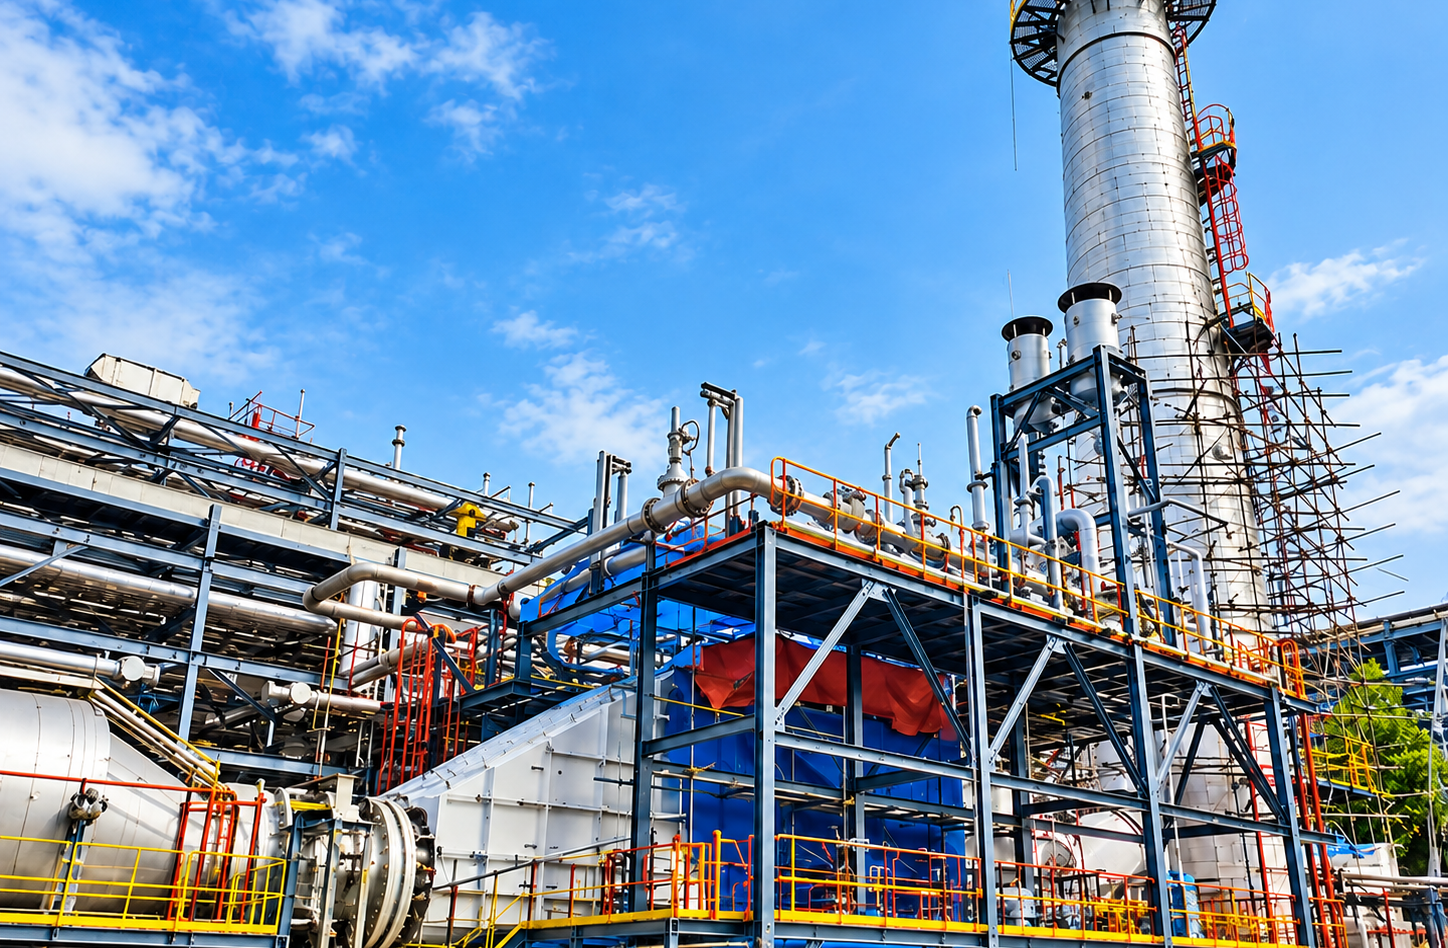
Tail gas leaving the SRU is thermally incinerated before discharge. The hot incinerator flue gas is cooled in a waste heat recovery boiler of fire tube or water tube construction.
Thermal Systems' incinerator packages are of modular construction for ease of site assembly, with references including a 600 TPD SRU at Essar, Vadinar.
For Sulphur Recovery Unit
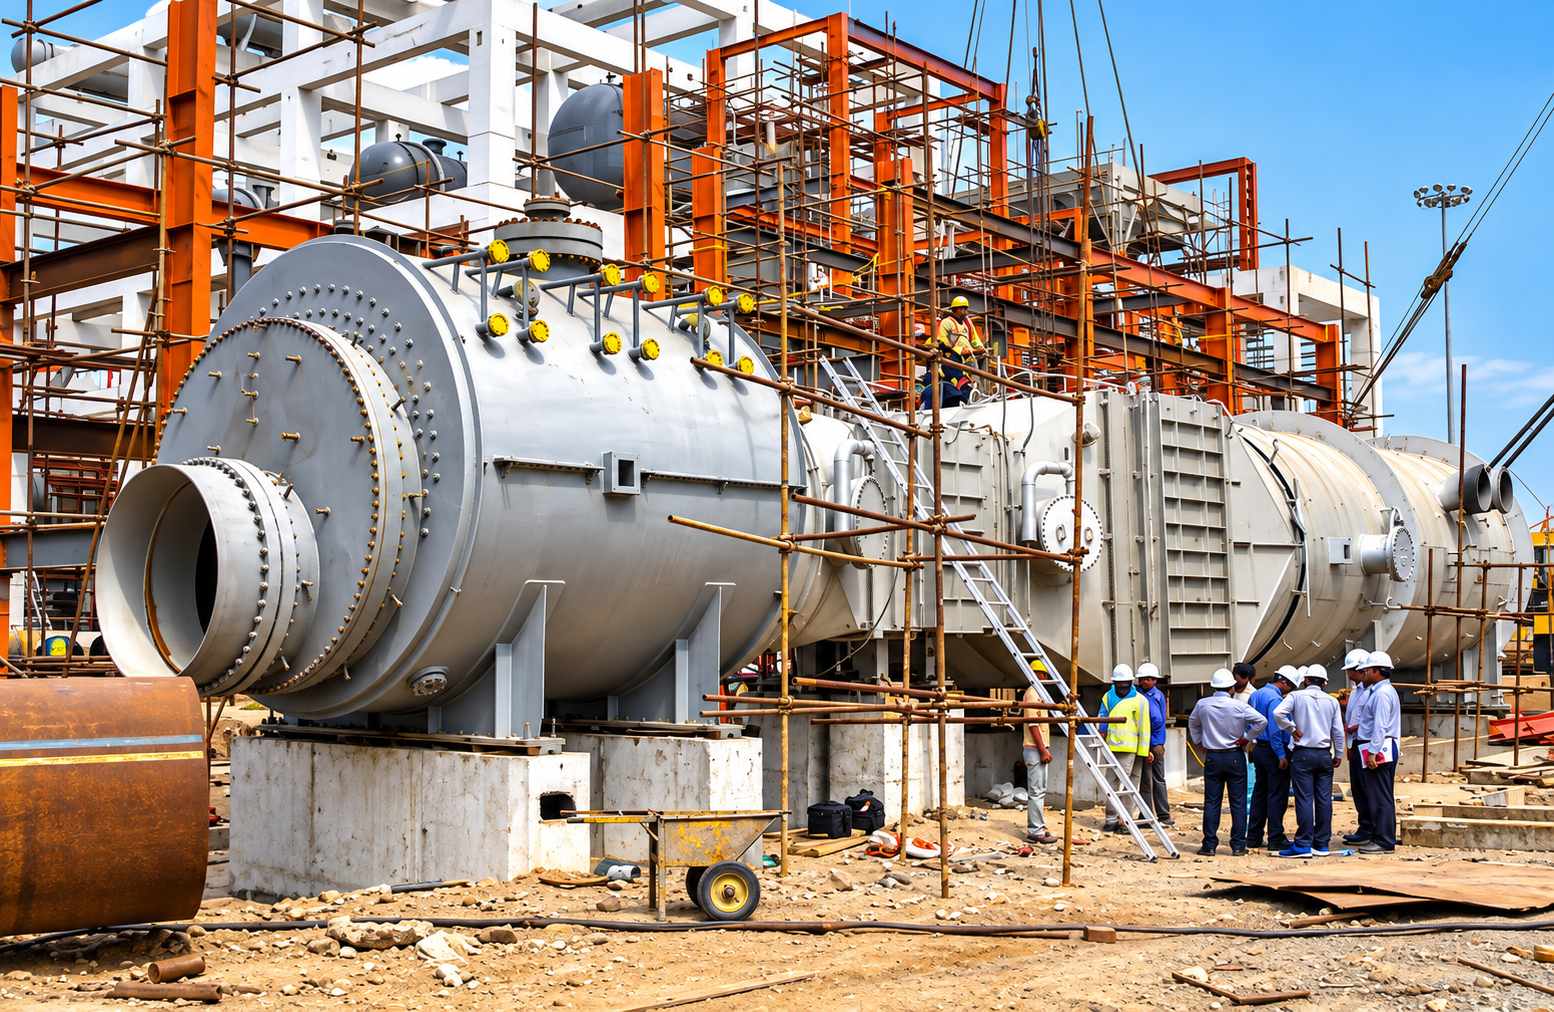
In tail gas treatment units, the treated gas stream is incinerated and its heat recovered in a waste heat boiler cum superheater.
Thermal Systems has supplied TGTU packages including 2 × 100 TPD TGTU boilers at HPCL Mumbai.